Image not available
Industrial manufacturing
HighEfficiency Gas Oil Hot Water Boiler Factory Leading China Suppliers
Looking for reliable China suppliers? Our factory provides high-performance gas oil hot water boilers with rated thermal power 0.7-140 MW, working pressure 0.7-1.25MP, and NOx emission ≤ 30mg. Compatible with natural gas, Lpg, biogas, and coke oven gas.
SupplierHEBEI HONGZE BOILER MANUFACTURING CO., LTD.www.hzsteamboiler.com
Source categories
About this product
Product information from the supplier.
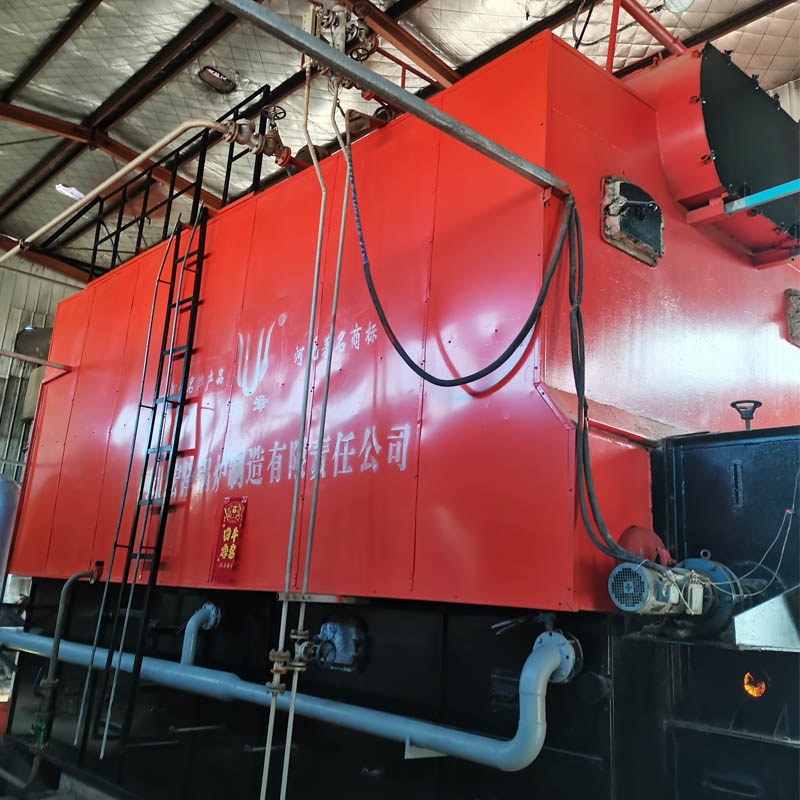
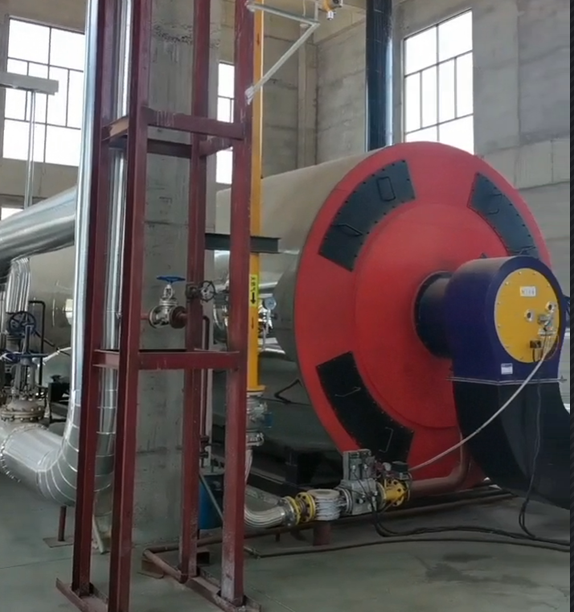
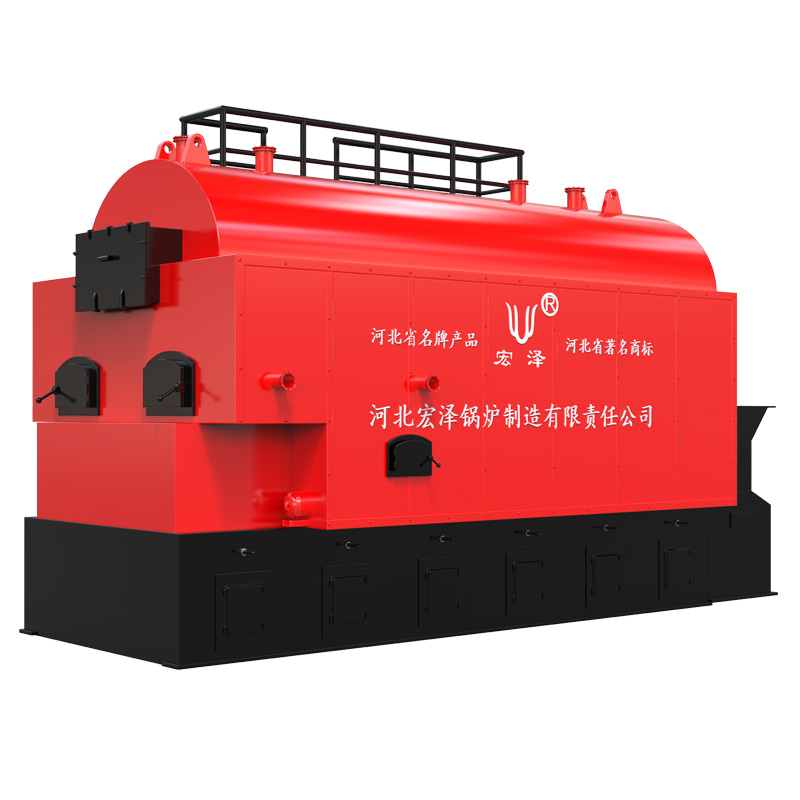
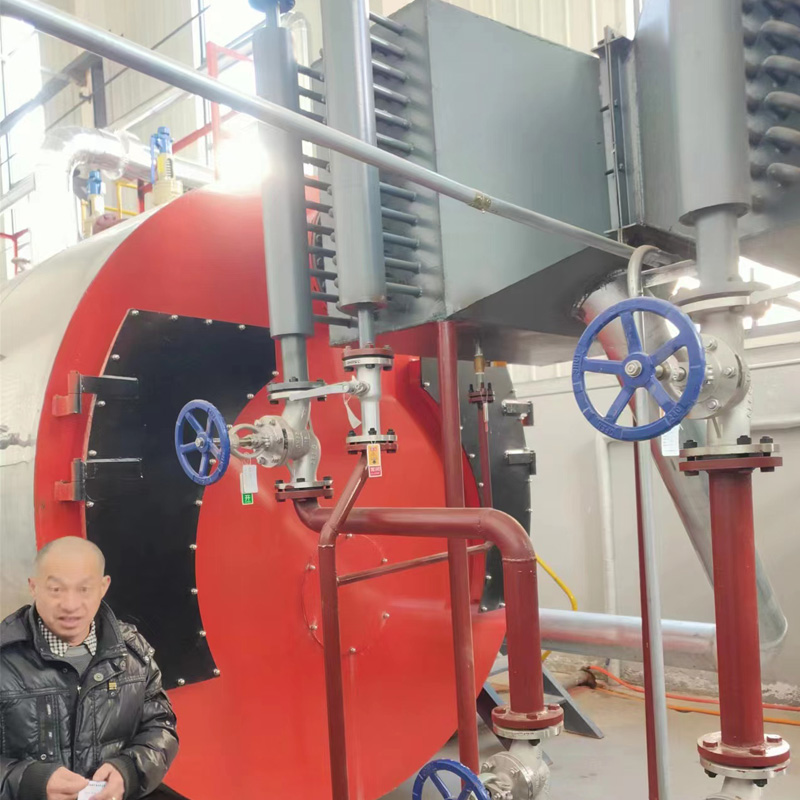
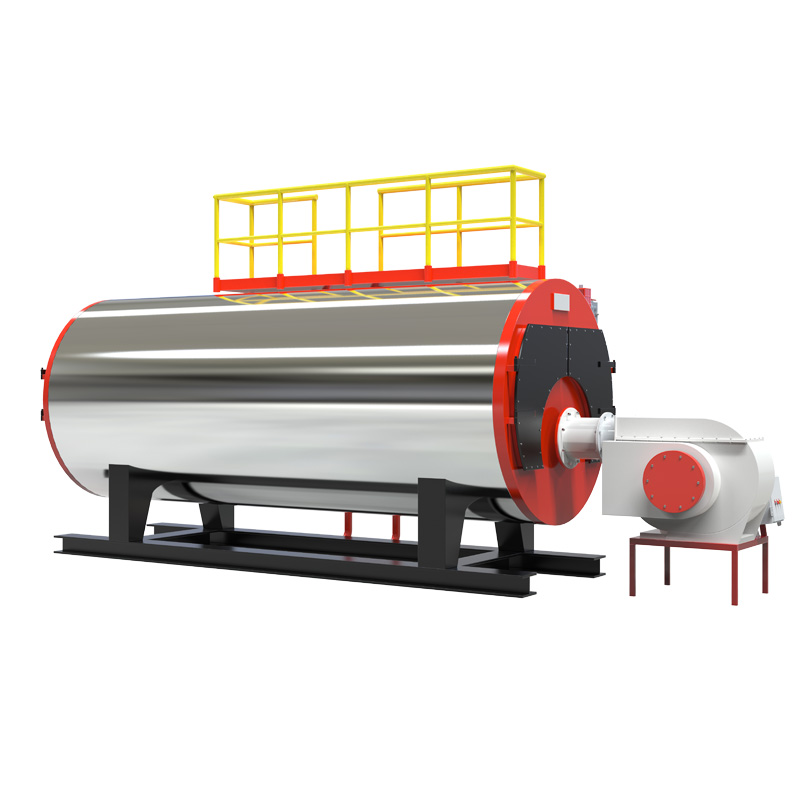
Our high-performance Gas (Oil) Hot Water Boilers are engineered for maximum thermal efficiency, utilizing advanced combustion principles to deliver consistent and reliable heating solutions. By converting the chemical energy of natural gas or oil into high-temperature hot water, these systems provide a stable heat source essential for industrial processing, commercial heating, and large-scale facility management.
Designed with a focus on sustainability and safety, our boilers integrate imported burner technology and sophisticated corrugated liners to minimize energy waste and emissions. From compact units for small-scale operations to massive industrial capacities up to 46MW, our range ensures a precise match for your specific thermal load requirements while maintaining strict environmental compliance.
Detailed Parameters
| Thermal Power Range | 0.7 MW - 46 MW | Max Working Pressure | Up to 1.25 MPa |
|---|---|---|---|
| Output Water Temp | 95℃ - 130℃ | Feeding Water Temp | 70℃ (Standard) |
| Max Thermal Efficiency | Up to 98.1% | NOx Emissions | ≤ 30mg/Nm³ |
| Fuel Compatibility | Natural Gas / Diesel Oil | Control System | Full-Automatic PLC |
| Energy Saving Tech | Corrugated Liner & Condenser | Safety Rating | Over-temp/Over-pressure Warning |
Key Advantages
Superior Thermal Efficiency
An expansive pot barrel heating area ensures full fuel combustion, maximizing heat transfer and reducing operational costs.
Eco-Friendly Emissions
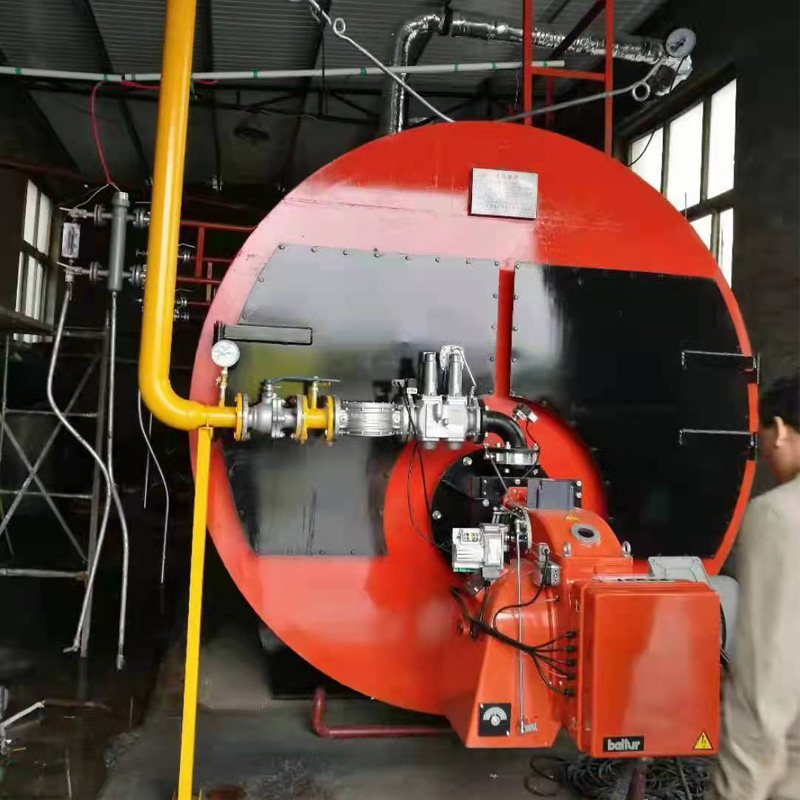
Equipped with premium imported burners to keep NOx emissions ≤30mg/Nm³, meeting the strictest global environmental standards.
Advanced Energy Recovery
Corrugated liners and threaded flue pipes work with condensers to recover waste heat, significantly lowering fuel consumption.
High-Sensitivity Safety
Professional gas valve groups provide instant leak detection and prevention to ensure a zero-accident working environment.
Intelligent Automation
A full-automatic control system monitors temperature and pressure in real-time, providing instant safety warnings.
Low Maintenance Load
Simplified structural design and modular components ensure that routine maintenance is fast, easy, and cost-effective.
Product Gallery
Management Platforms
Thermal Load Balancing
Precision management of heat output to match real-time demand, preventing energy waste.
Combustion Optimization
Automatic air-fuel ratio adjustment to ensure complete combustion and peak efficiency.
Real-time Safety Alerts
Instant notification systems for over-pressure or over-temperature events to prevent downtime.
Emission Monitoring
Digital tracking of NOx and flue gas temperatures to ensure environmental compliance.
Predictive Maintenance
System logs and performance tracking to schedule maintenance before failures occur.
Remote Control Interface
Centralized management platform for operating multiple boiler units from a single hub.
Investment Return Comparison
| Performance Metric | Standard Boiler | Our High-Efficiency Boiler |
|---|---|---|
| Avg. Thermal Efficiency | 85% - 89% | 94% - 98% |
| Annual Fuel Cost | Baseline (100%) | Reduced by 12-15% |
| NOx Emission Levels | Medium/High | Ultra-Low (≤30mg/Nm³) |
| Maintenance Cycle | Frequent | Extended / Predictive |
| ROI Period | 4-6 Years | 2-3 Years |
Frequently Asked Questions
Q: What is the primary difference between a steam boiler and a hot water boiler?
A steam boiler produces steam for heating or industrial processes, while a hot water boiler heats water to a specific temperature (usually below boiling) to be circulated through a heating system.
Q: How does the corrugated liner improve efficiency in your boilers?
The corrugated liner increases the heat transfer surface area and creates turbulence in the flue gas, which enhances heat absorption and reduces exhaust gas temperature.
Q: Can these boilers switch between gas and oil fuel?
Yes, our dual-fuel capable models are designed to operate on either natural gas or oil, providing flexibility in fuel procurement and operational continuity.
Q: What safety measures are included to prevent gas leaks?
Our systems feature high-sensitivity gas valve groups and an automated control system that triggers immediate shutdowns and warnings upon detecting pressure anomalies or leaks.
Q: How is the thermal efficiency of 98.1% achieved?
This is achieved through a combination of a large heating area, high-precision imported burners, threaded flue pipes, and an integrated condenser system that recovers latent heat.
Q: What is the expected lifespan of these industrial boilers?
With proper water treatment and adherence to the recommended maintenance schedule, our boilers are designed for a long industrial lifespan, typically exceeding 15-20 years.
Ready to Optimize Your Industrial Heating Efficiency?
Contact UsMore from this supplier
HEBEI HONGZE BOILER MANUFACTURING CO., LTD.