Image not available
Industrial manufacturing
High Performance Submerged Arc Welding SAW Wire Factory and Suppliers in China
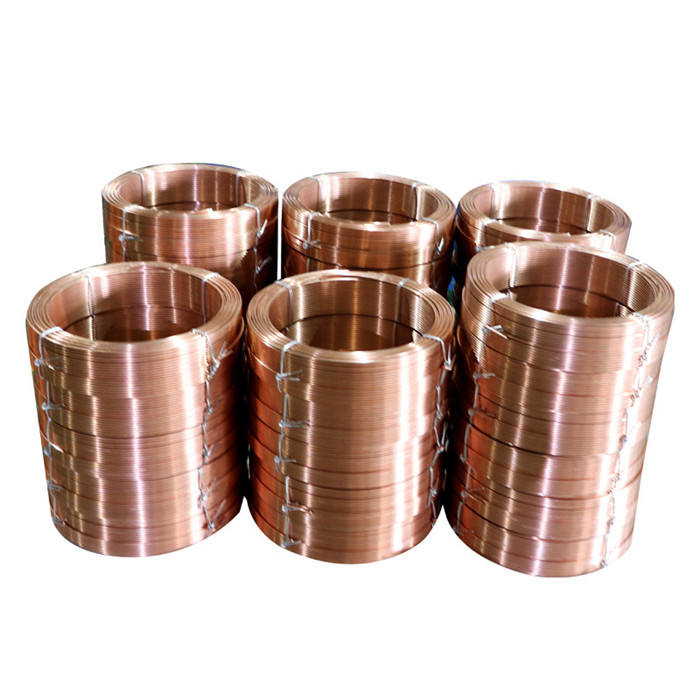
Looking for high-quality SAW wires? As leading China suppliers and a professional factory, we provide premium submerged arc welding wires for carbon steel, ensuring high stability and superior weld quality for boilers and ships.
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
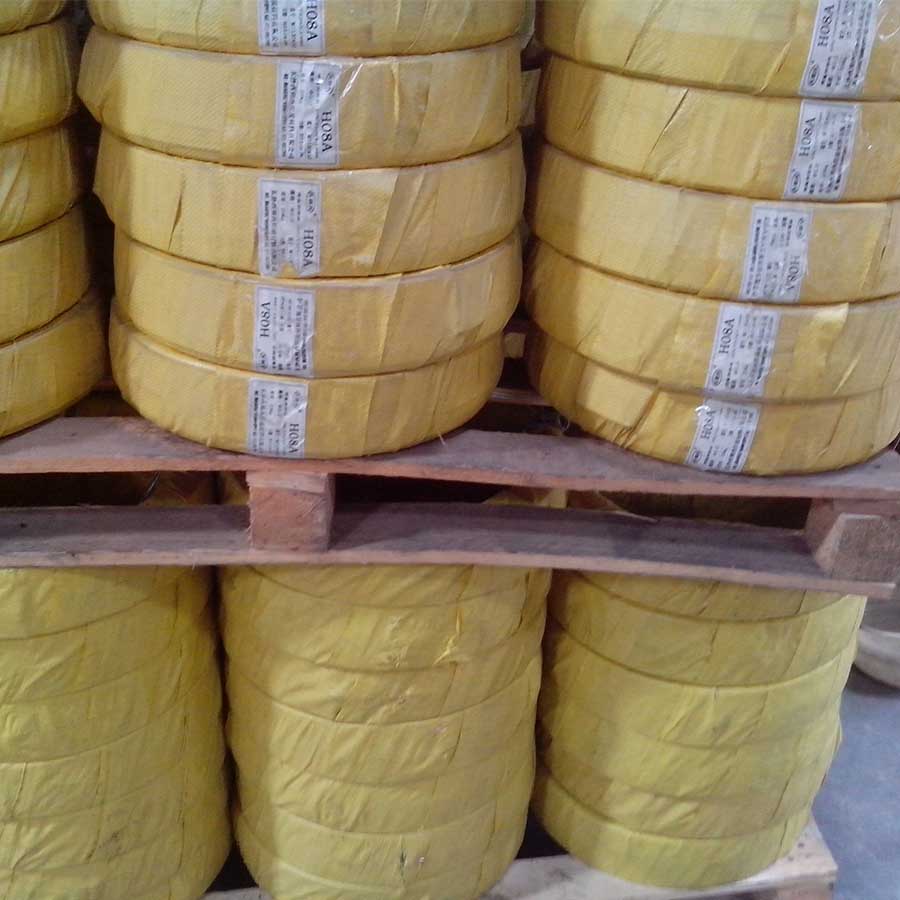
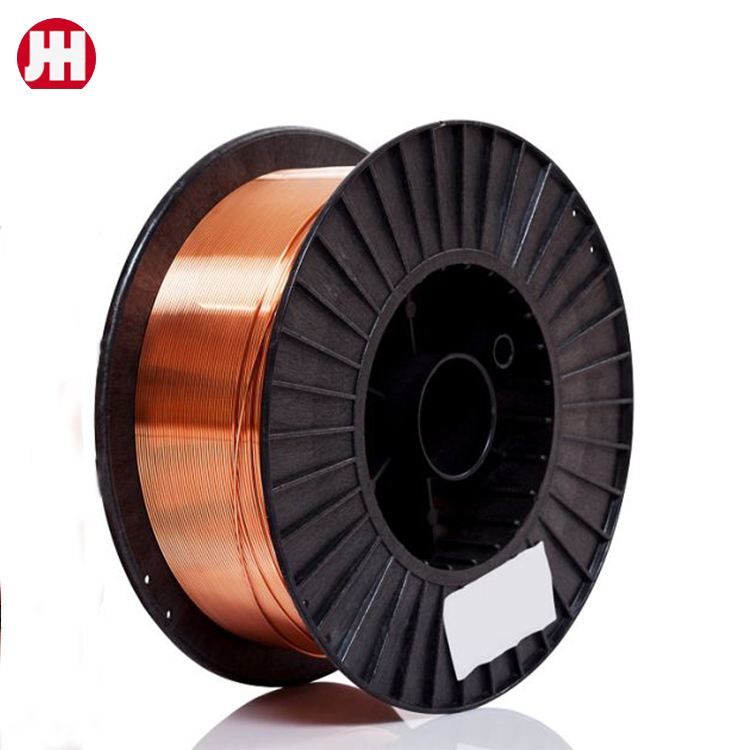
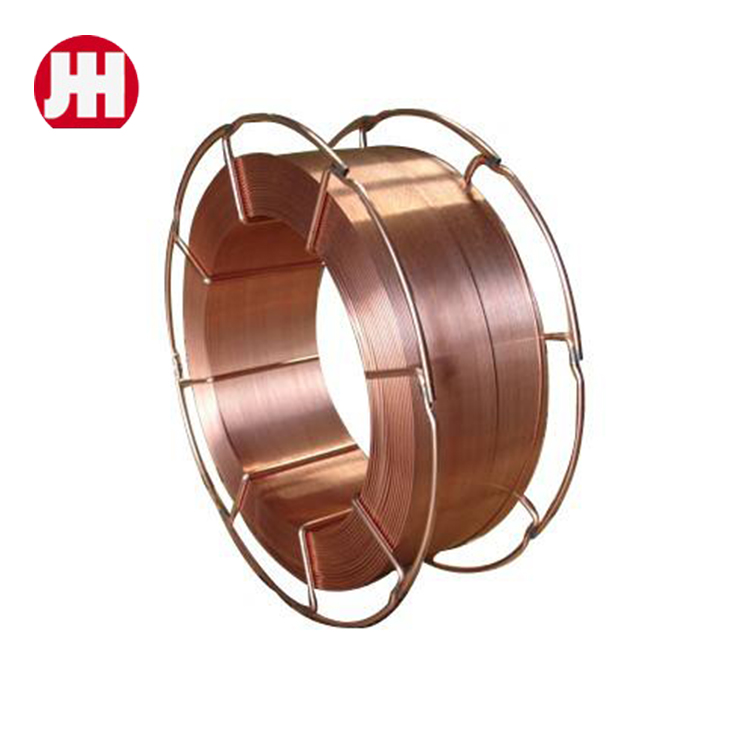
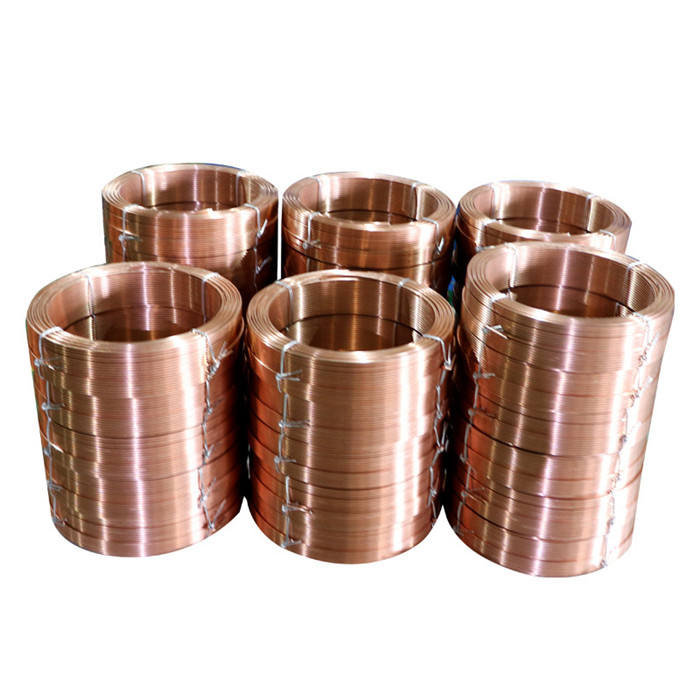
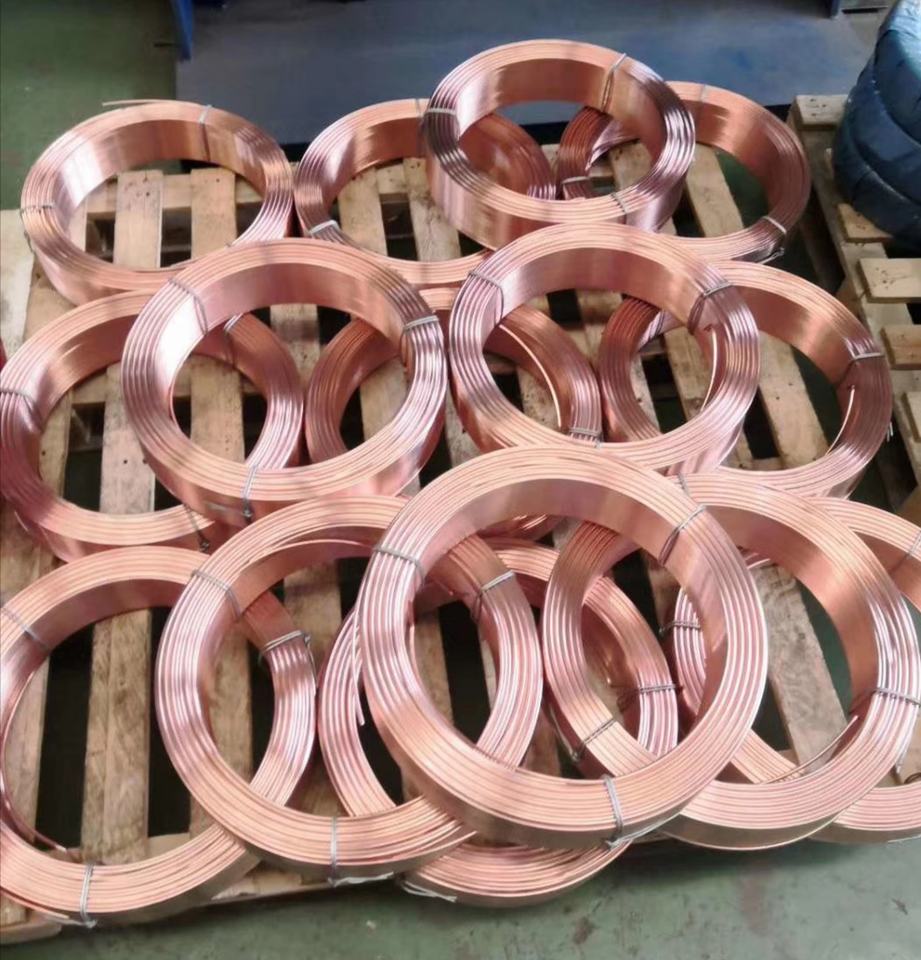
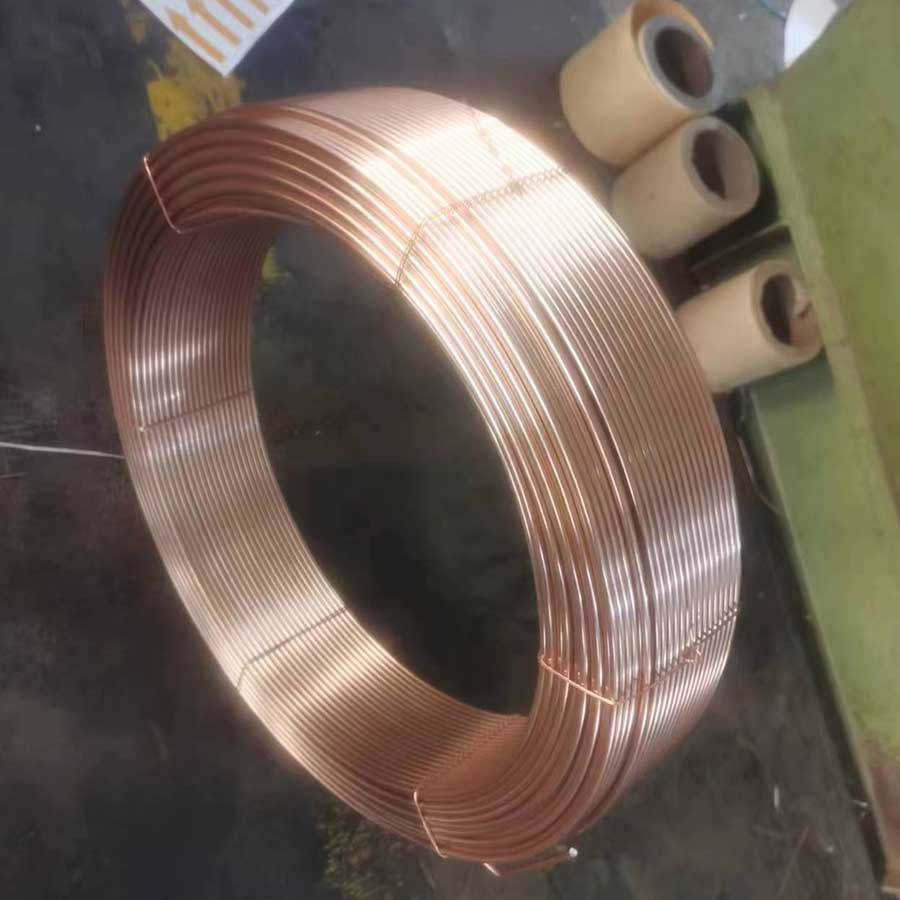
Our Submerged Arc Welding (SAW) wires are engineered for high-performance carbon steel welding, providing a superior solution for industries requiring exceptional stability and high-quality weld seams. Designed for workpieces with stringent structural requirements, our SAW consumables ensure a high-density weld with consistent mechanical properties across various industrial applications.
Combining advanced metallurgical compositions with precise manufacturing, these welding wires offer excellent weldability and high deposition efficiency. Whether you are working with low-carbon steel structures or high-strength alloy steels, our range of SAW wires—including H08A and H08MnA—provides the stability and strength needed for critical infrastructure projects.
Detailed Parameters
| Product Grade | H08A / H08MnA / H10Mn2 / H10MnSi | Material Type | Carbon Steel / Low-Alloy Steel |
|---|---|---|---|
| Application | Boilers, Ships, Pressure Vessels, Pipelines | Weld Strength | 300-350MPa (for H08MnA) |
| Compatible Flux | SJ301, HJ431, and similar grades | Compatible Steel | Q235, 20#, Q195, Q215 |
| Flux Baking Temp | Sintering: 300-350℃ / Smelting: 200-250℃ | Baking Duration | 1-2 Hours before application |
| Storage Temp | Above 5°C (Indoor) | Storage Humidity | Relative Humidity ≤ 60% |
Key Advantages
Superior Weldability
Engineered for excellent mechanical properties and stable arc performance during high-demand welding processes.
High Efficiency
Optimized for high deposition efficiency, significantly reducing production time and labor costs.
Stable Arc Quality
Maintains a steady arc to ensure consistent weld penetration and high-quality structural integrity.
Easy Slag Removal
Formulated for quick and easy slag separation, reducing post-weld cleaning and finishing time.
Perfect Bead Shape
Produces smooth, aesthetically pleasing weld beads that meet strict industrial inspection standards.
Versatile Application
Compatible with a wide range of carbon steels, from low-carbon Q235 to high-strength structural steel.
Product Gallery
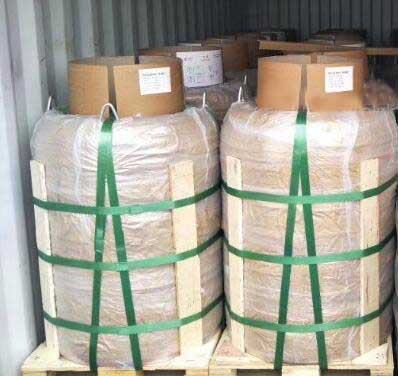
Management Platforms
Inventory Tracking
Real-time monitoring of welding wire stock to ensure seamless production cycles.
Process Optimization
Customized welding specifications based on specific material and energy input.
Quality Alerts
Instant notifications for flux baking schedules and storage humidity thresholds.
Compliance Audit
Full traceability for batch numbers to meet international welding standards.
Storage Control
Strict indoor climate management (Temp > 5°C) to prevent moisture contamination.
Technical Support
Expert guidance on matching H08A or H08MnA wires to your specific steel grade.
Investment Return Comparison
| Performance Metric | Standard SAW Wire | Our Premium SAW Wire |
|---|---|---|
| Deposition Rate | Moderate | High Efficiency |
| Weld Stability | Variable | Consistently Stable |
| Slag Removal Time | Standard | Rapid / Easy |
| Mechanical Strength | Basic | Enhanced (up to 350MPa) |
| Waste Material Rate | Normal | Low / Optimized |
Frequently Asked Questions
Q: What is the difference between H08A and H08MnA submerged welding wires?
H08A is typically used for low-carbon steel where strength requirements are lower, while H08MnA has a higher Manganese content, making it suitable for high-quality carbon steel and low-alloy structural steel with strength levels of 300-350MPa.
Q: How should I bake the flux before using it with submerged arc welding wire?
Flux should be baked for 1-2 hours. Sintering flux requires a temperature of 300-350℃, while smelting flux should be baked at 200-250℃ to ensure optimal performance.
Q: What are the ideal storage conditions for SAW welding consumables?
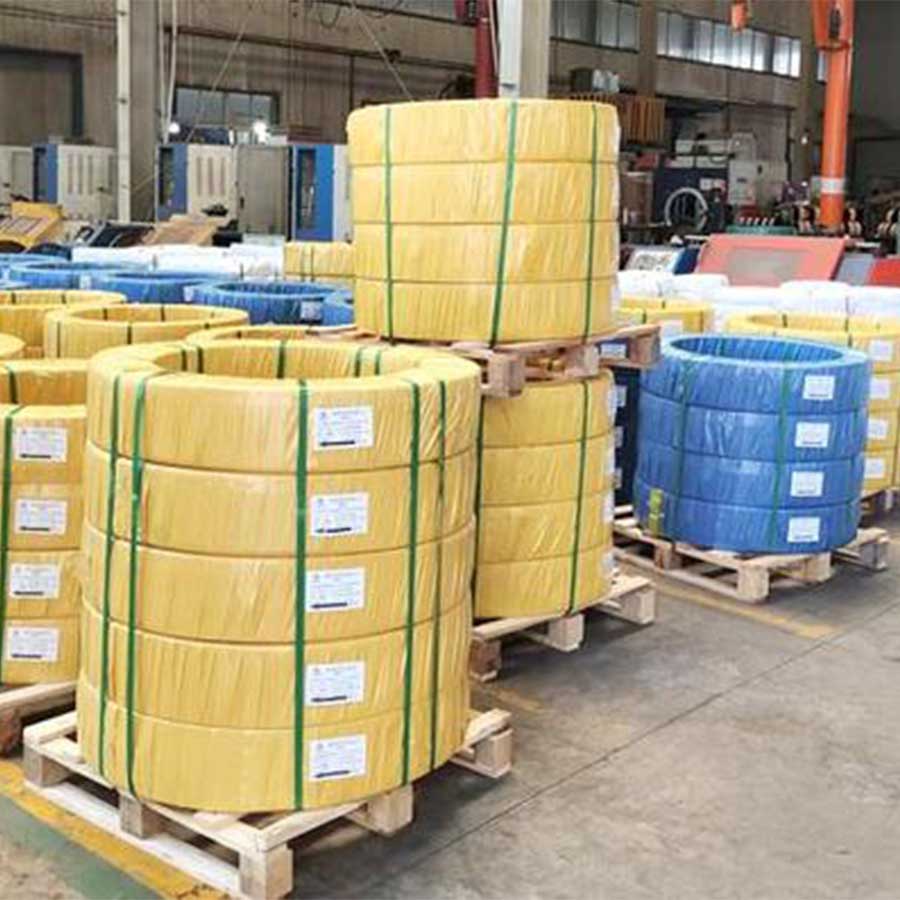
They should be stored indoors at temperatures above 5°C with relative humidity below 60%. Maintain a distance of at least 300mm from floors and walls.
Q: How do I prepare the welding surface for submerged arc welding?
All rust, oil, moisture, and other impurities must be thoroughly removed from the welding surface and the welding wire itself before starting the process.
Q: Which industries commonly use submerged arc welding wires?
It is widely utilized in the manufacturing of boilers, shipbuilding, pressure vessels, and large-scale pipeline construction due to its high stability and weld quality.
Q: Does the welding energy input affect the final weld properties?
Yes, the energy input directly impacts the mechanical properties of the weld metal. We recommend conducting a process evaluation to formulate the appropriate specifications for your specific conditions.
Ready to Upgrade Your Welding Precision?
Contact UsNeed a quick quotation for submerged arc welding wire? Chat with us on WhatsApp or email info@steeltoolschina.com.
See the full submerged arc welding wire range, or browse all copper coated welding wire.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.