Image not available
Non-metallic minerals
High Purity Refined Industrial Salt Factory and Suppliers in China
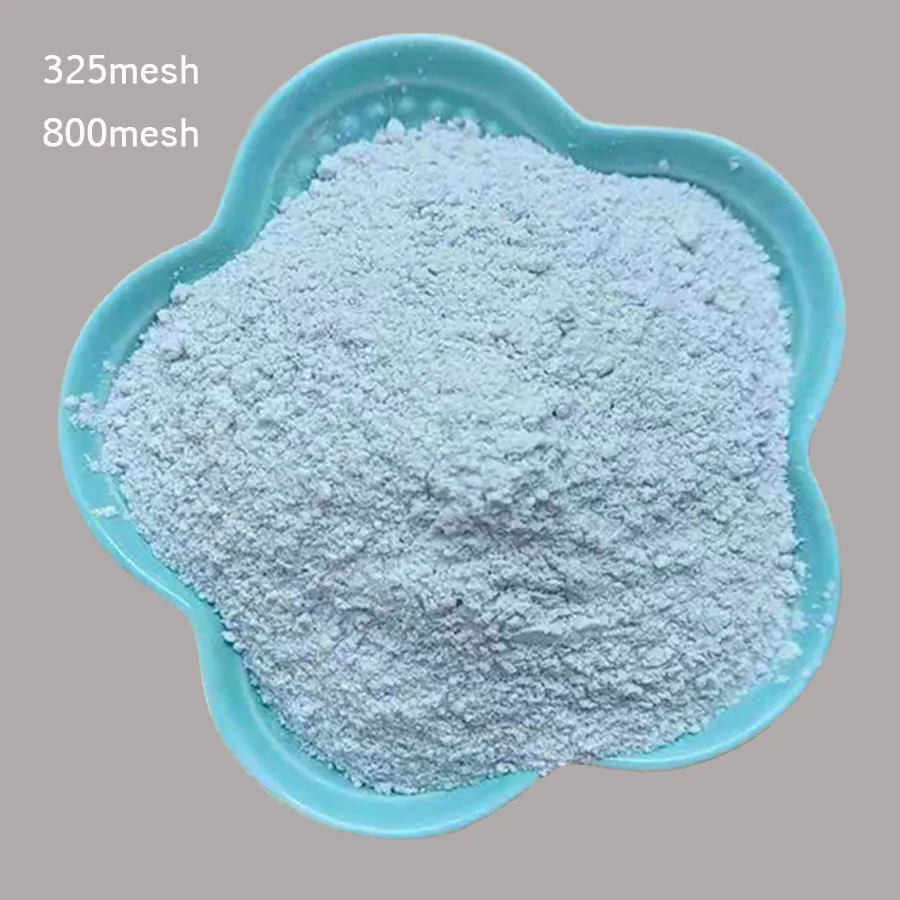
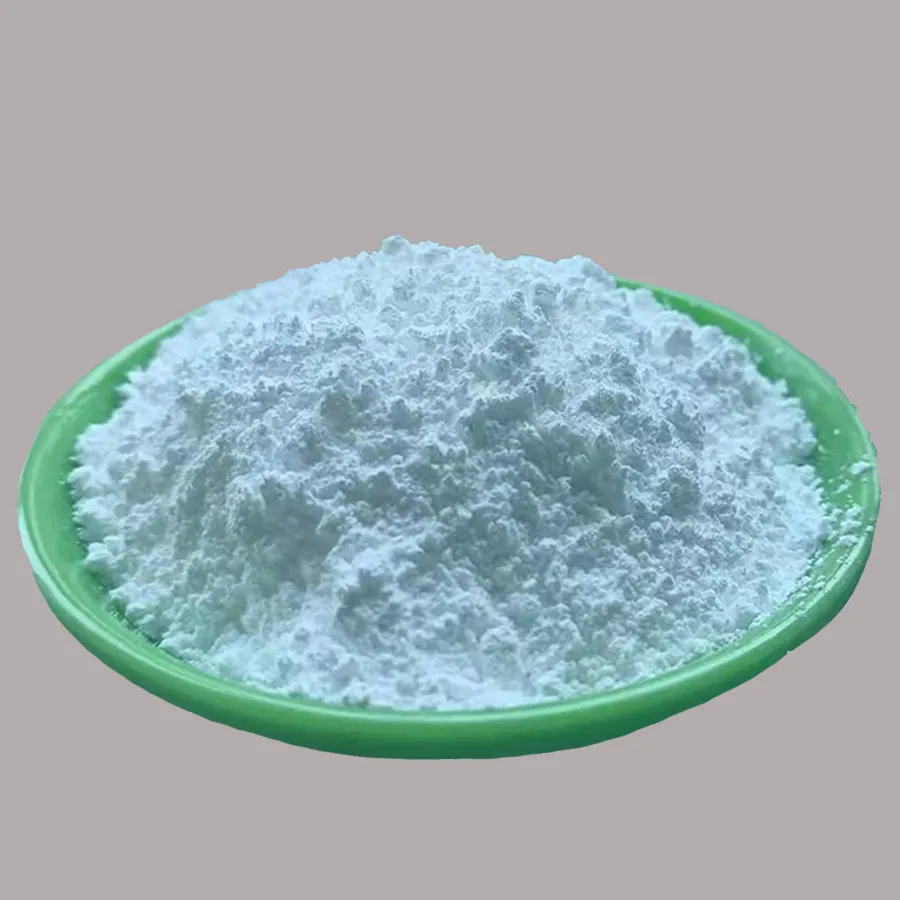
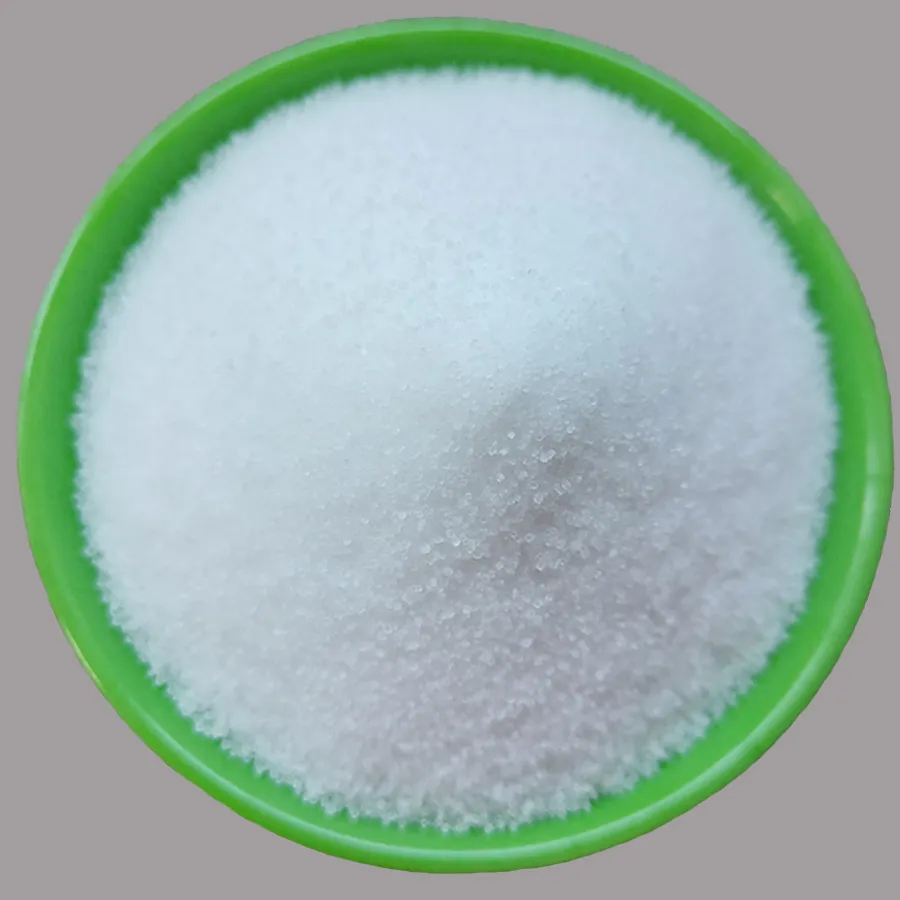
Premium Refined Industrial Salt from a leading China factory. High purity white powder, 20-200 mesh, ideal for chemical synthesis and water treatment. Contact top suppliers for bulk orders.
SupplierShijiazhuang Baifeng Mining Co.,Ltdwww.baifengmining.com
Source categories
About this product
Product information from the supplier.
Our Refined Industrial Salt is a high-purity sodium chloride solution engineered to meet the rigorous demands of modern industrial processing. Sourced from premium mineral deposits and subjected to advanced purification techniques, this product ensures consistent chemical stability and minimal impurity levels, making it an essential raw material for chemical synthesis, water treatment, and textile manufacturing.
Designed for maximum solubility and operational efficiency, our refined salt minimizes equipment scaling and prevents catalyst poisoning in sensitive industrial reactions. Whether used in the production of chlorine and caustic soda or as a critical agent in food processing and pharmaceuticals, our industrial salt provides the reliability and purity required to optimize your production yield and maintain strict quality control standards.
Detailed Parameters
| Chemical Composition | NaCl ≥ 99.5% | Physical Form | Crystalline Powder/Granular |
|---|---|---|---|
| Moisture Content | ≤ 0.1% | Appearance | Pure White |
| Insoluble Matter | ≤ 0.02% | pH Value | 6.5 - 7.5 |
| Calcium/Magnesium | Ultra-Low Trace | Particle Size | Customizable |
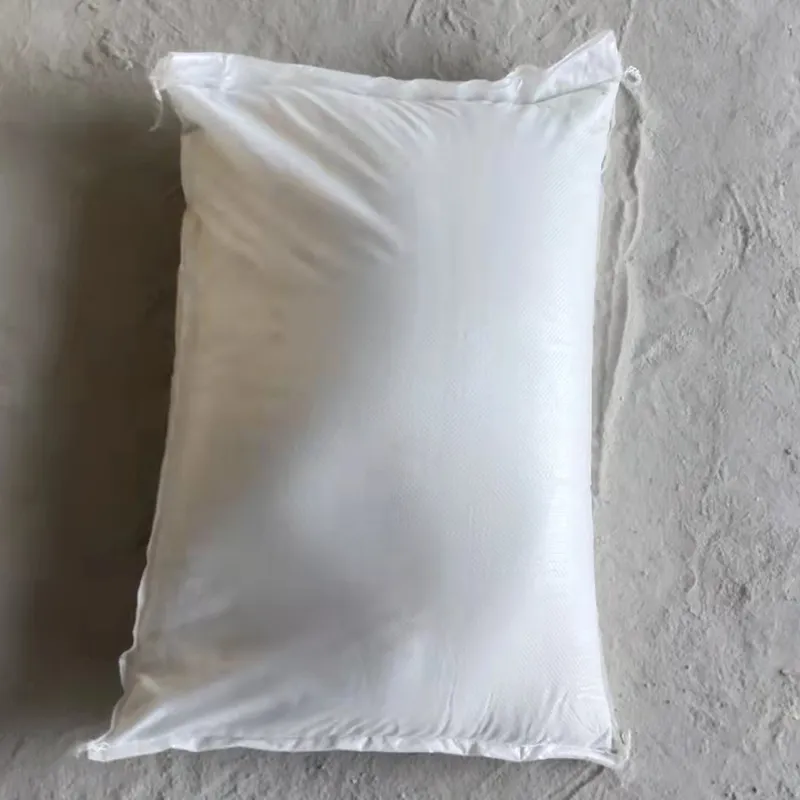
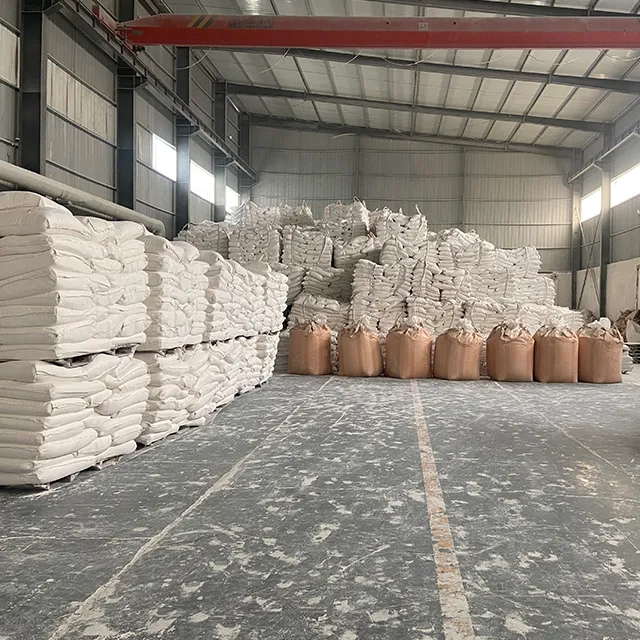
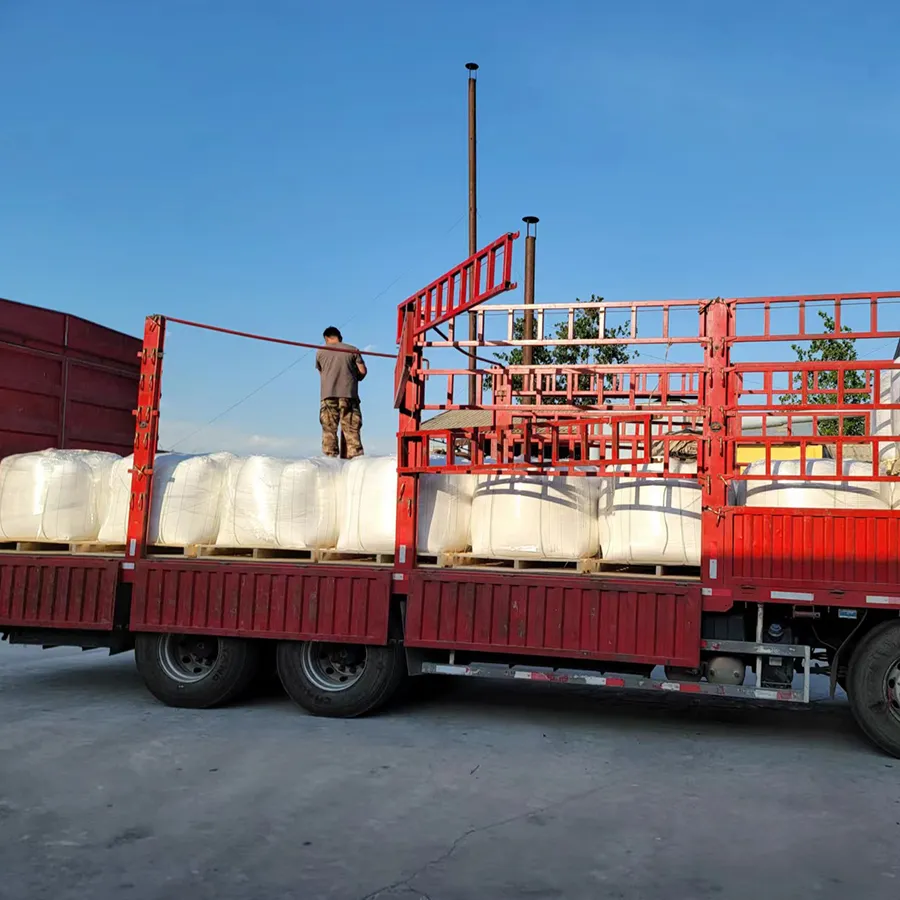
| Packaging | 25kg/50kg Bags / Jumbo Bags | Standard Compliance | Industrial Grade / ISO Standard |
Key Advantages
Ultra-High Purity
Rigorous refining processes ensure minimum impurities, preventing contamination in high-precision chemical reactions.
Rapid Solubility
Optimized crystal structure allows for fast dissolution, reducing energy consumption and processing time.
Consistent Quality
Strict batch-to-batch monitoring ensures that every shipment meets the exact specifications of your production line.
Equipment Protection
Low mineral residue prevents scale build-up in pipes and tanks, extending the lifespan of your hardware.
Versatile Application
Perfectly suited for diverse sectors including textiles, soaps, metallurgy, and water softening systems.
Eco-Friendly Sourcing
Extracted and processed using sustainable mining practices to reduce the overall environmental footprint.
Product Gallery
Management Platforms
Inventory Control
Real-time monitoring of salt reserves to ensure an uninterrupted supply chain for your plant.
Quality Assurance
Integrated laboratory testing for every batch to verify purity and chemical composition.
Logistics Tracking
Advanced GPS tracking and notification systems for precise delivery scheduling.
Order Automation
Simplified digital procurement platform to reduce lead times and administrative errors.
Storage Optimization
Guidance on moisture-proof warehousing to maintain product integrity over long periods.
Regulatory Support
Full documentation and MSDS provision to comply with international safety standards.
Investment Return Comparison
| Metric | Standard Industrial Salt | Our Refined Industrial Salt |
|---|---|---|
| Purity Level | 95% - 98% | ≥ 99.5% |
| Processing Speed | Baseline | 15% Faster Dissolution |
| Equipment Wear | Moderate Scaling | Minimal Residue |
| Waste Generation | Higher Impurity Sludge | Ultra-Low Waste |
| Overall Efficiency | Standard Yield | Enhanced Product Yield |
Frequently Asked Questions
Q: What are the primary applications of Refined Industrial Salt?
It is widely used in chlor-alkali plants for producing chlorine and caustic soda, in textile dyeing for fixing colors, and in water softening systems to remove hardness minerals.
Q: How does refined salt differ from raw rock salt?
Refined salt undergoes extensive purification to remove insoluble minerals like calcium and magnesium, resulting in much higher purity and better solubility than raw rock salt.
Q: Can you provide customized particle sizes for specific machinery?
Yes, we offer a variety of grades ranging from fine powder to coarse granules to ensure compatibility with your specific industrial equipment and dissolution rates.
Q: What is the shelf life of the refined industrial salt?
When stored in a cool, dry environment and protected from moisture in airtight packaging, our refined salt has an almost indefinite shelf life.
Q: Does your product meet international quality standards?
Absolutely. Our production process adheres to strict ISO quality management standards, and we provide comprehensive certificates of analysis (COA) for every shipment.
Q: What packaging options are available for bulk orders?
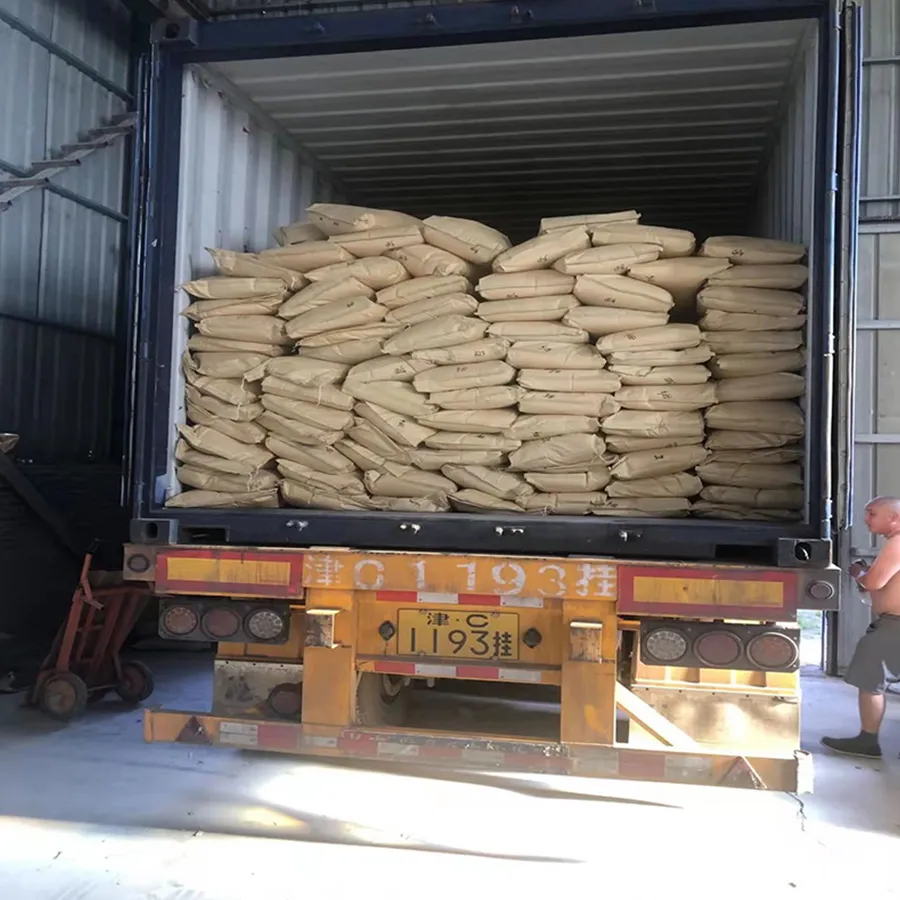
We provide flexible packaging options including 25kg and 50kg woven PP bags, as well as 1-ton jumbo bags for large-scale industrial operations.
Ready to Optimize Your Industrial Production with High-Purity Salt?
Contact UsMore from this supplier
Shijiazhuang Baifeng Mining Co.,Ltd