Image not available
Industrial manufacturing
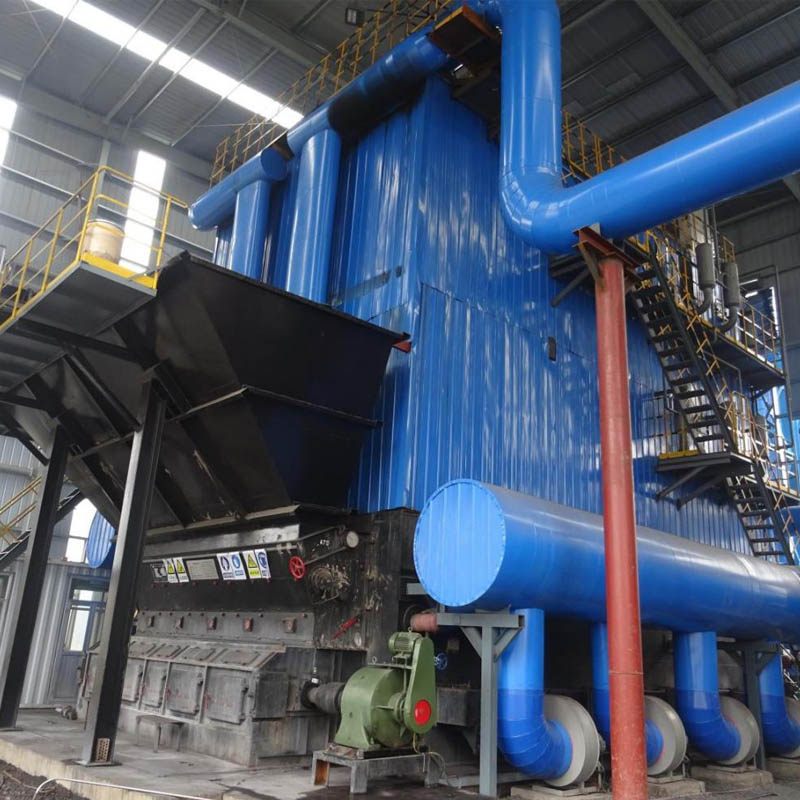
HighEfficiency Coal Fired Thermal Oil Boiler China Factory Suppliers
Looking for reliable China suppliers? Our factory provides high-performance coal fired thermal oil boilers with 95% efficiency, 320°C outlet temp, and 0.8-1.0 MPa pressure. Ideal for lignite, anthracite, and bituminous coal to optimize industrial heating.
SupplierHEBEI HONGZE BOILER MANUFACTURING CO., LTD.www.hzsteamboiler.com
Source categories
About this product
Product information from the supplier.
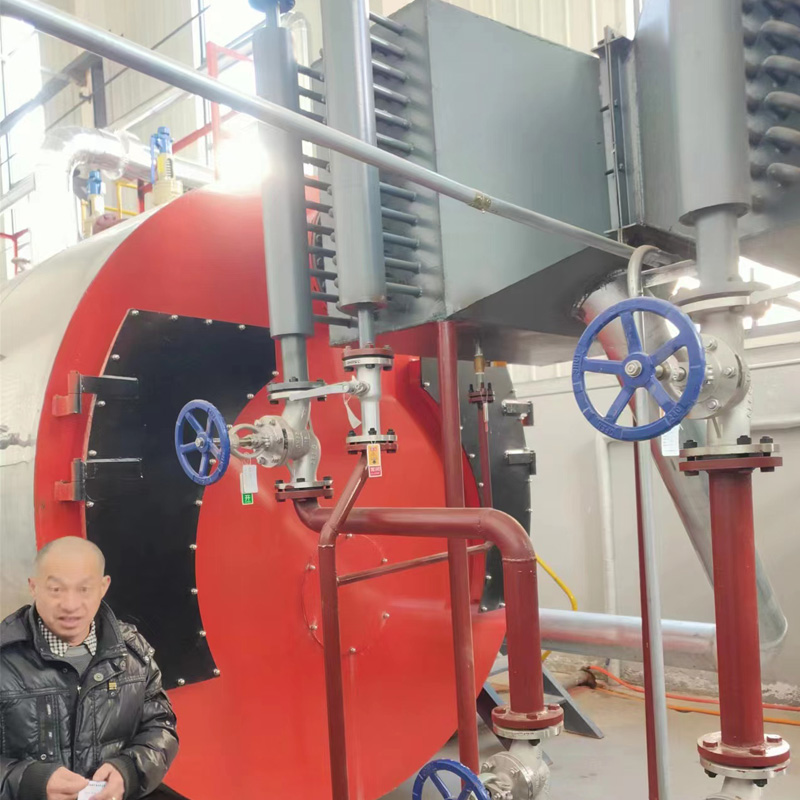
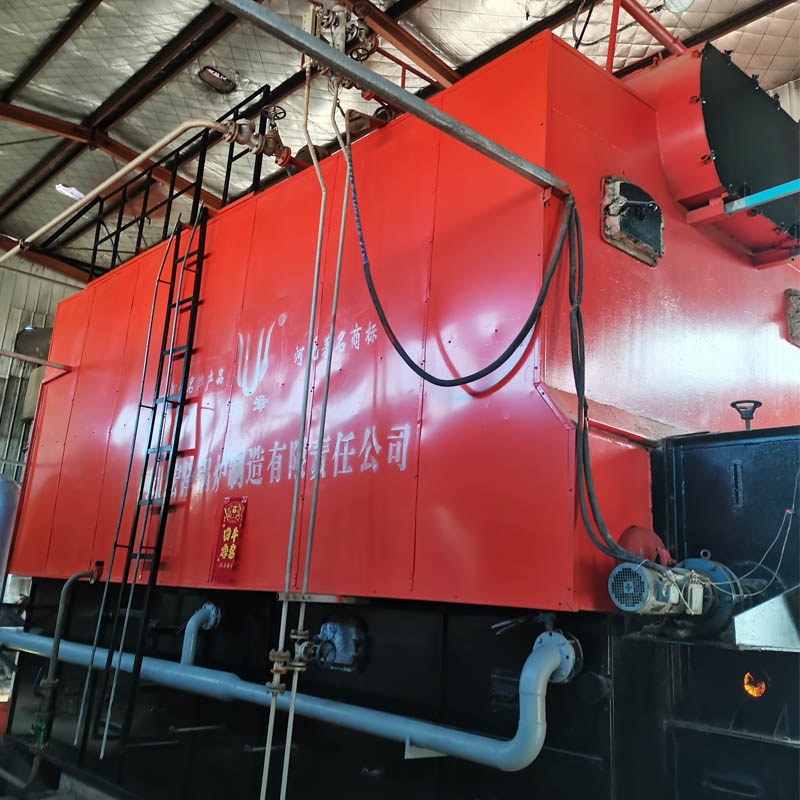
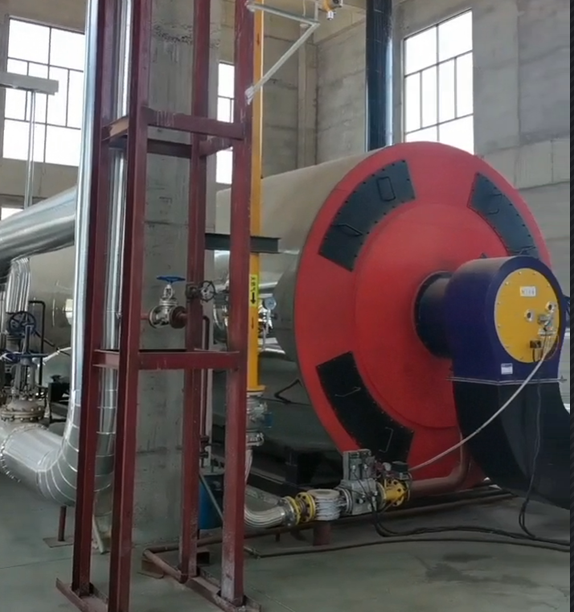
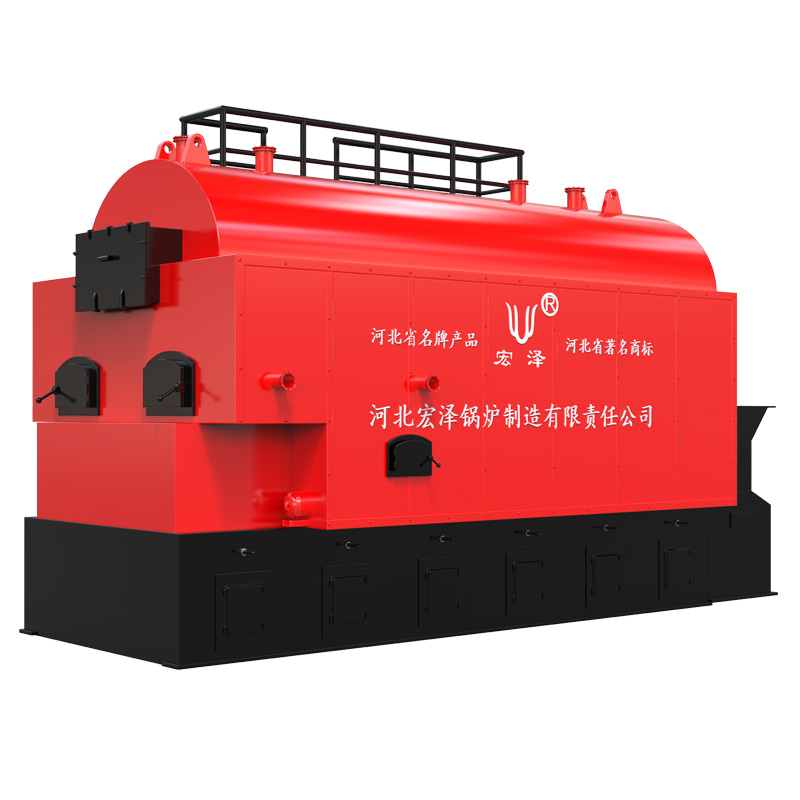
The Coal Fired Thermal Oil Boiler is a high-performance industrial heating solution engineered for applications requiring high-temperature heat transfer with minimal operating pressure. By utilizing a specialized liquid-phase heat carrier, this system ensures uniform heat distribution and eliminates the risks associated with high-pressure steam, making it an ideal choice for complex industrial thermal processes.
Designed for maximum efficiency and stability, our thermal oil boilers feature a closed-loop heating system that significantly reduces energy waste. Whether replacing water-poor steam boilers or powering large-scale manufacturing lines, this equipment provides precise temperature control and robust safety detection, ensuring sustainable and reliable thermal energy management for your facility.
Detailed Parameters
| Design Working Temp | ≤ 320 ℃ | Rated Working Pressure | 1 Mpa |
|---|---|---|---|
| Thermal Efficiency | ≥ 95% | Heat Transfer Medium | Thermal Oil (Liquid Phase) |
| Power Range (Kw) | 350 - 4000 Kw | Capacity Range (m³) | 0.3 - 4.5 m³ |
| Heat Output (10⁴Kcal/h) | 30 - 350 10⁴Kcal/h | Control System | Full Operation & Safety Detection |
| Heating Method | Closed Loop / Liquid Phase | Application | Industrial Heating Replacement |
Key Advantages
Low Pressure, High Temp
Capable of achieving superior working temperatures while maintaining significantly lower operating pressures for enhanced safety.
Precise Temp Control
Ensures stable heating and highly accurate temperature adjustments to meet rigorous industrial process requirements.
Maximized Efficiency
Optimized thermal efficiency is maintained across various working conditions to lower operational fuel costs.
Advanced Safety
Equipped with a comprehensive suite of operation control and safety detection devices for worry-free monitoring.
Liquid-Phase Transfer
Utilizes efficient liquid-phase heat transfer for more consistent energy distribution compared to traditional steam.
Closed Loop System
Features a closed-loop heating architecture that ensures high heat utilization and minimal environmental loss.
Product Gallery
Management Platforms
Thermal Load Monitoring
Real-time tracking of thermal output to optimize fuel consumption and heat delivery.
Pressure Regulation
Automated control systems to maintain the ideal low-pressure environment during high-heat cycles.
Safety Alert System
Instant notification for any parameter deviations through the integrated safety detection unit.
Temp Precision Logic
Sophisticated algorithms to ensure the heat carrier remains at the exact design temperature.
Oil Level Control
Smart monitoring of thermal oil capacity to prevent dry-run and ensure pump longevity.
Cycle Optimization
Closed-loop flow management to increase the overall utilization rate of the thermal energy.
Investment Return Comparison
| Feature | Traditional Steam Boiler | Thermal Oil Boiler |
|---|---|---|
| Operating Pressure | High Pressure (Risky) | Low Pressure (Safe) |
| Temperature Stability | Fluctuating | Highly Precise |
| Heat Utilization | Moderate (Losses) | High (Closed Loop) |
| Water Requirements | High Purity Water | Low/No Water Needed |
| Energy Efficiency | Standard | Optimized (Up to 95%) |
Frequently Asked Questions
Q: What are the primary benefits of a Thermal Oil Boiler over a Steam Boiler?
Thermal oil boilers can achieve much higher temperatures at significantly lower pressures, reducing safety risks and eliminating the need for expensive high-pressure vessels and water treatment.
Q: How does the closed-loop system improve energy efficiency?
The closed-loop system recirculates the heat carrier, minimizing heat loss to the atmosphere and ensuring that almost all generated energy is delivered directly to the production equipment.
Q: Is this boiler suitable for areas with limited water supply?
Yes, it is specifically designed to replace water-dependent steam boilers, making it an excellent solution for water-poor regions or industries looking to reduce water consumption.
Q: What is the typical thermal efficiency of these units?
Our coal-fired thermal oil boilers are engineered to maintain a high thermal efficiency of ≥ 95% across various operating conditions.
Q: What safety mechanisms are included in the boiler?
The system includes comprehensive operation control and safety detection devices, including pressure monitors and temperature alarms to ensure secure industrial operation.
Q: Can the temperature be adjusted precisely for different products?
Absolutely. The system allows for precise temperature adjustment, enabling users to switch between different heating requirements with high stability.
Ready to Optimize Your Industrial Heating Efficiency?
Contact UsMore from this supplier
HEBEI HONGZE BOILER MANUFACTURING CO., LTD.