Image not available
Industrial manufacturing
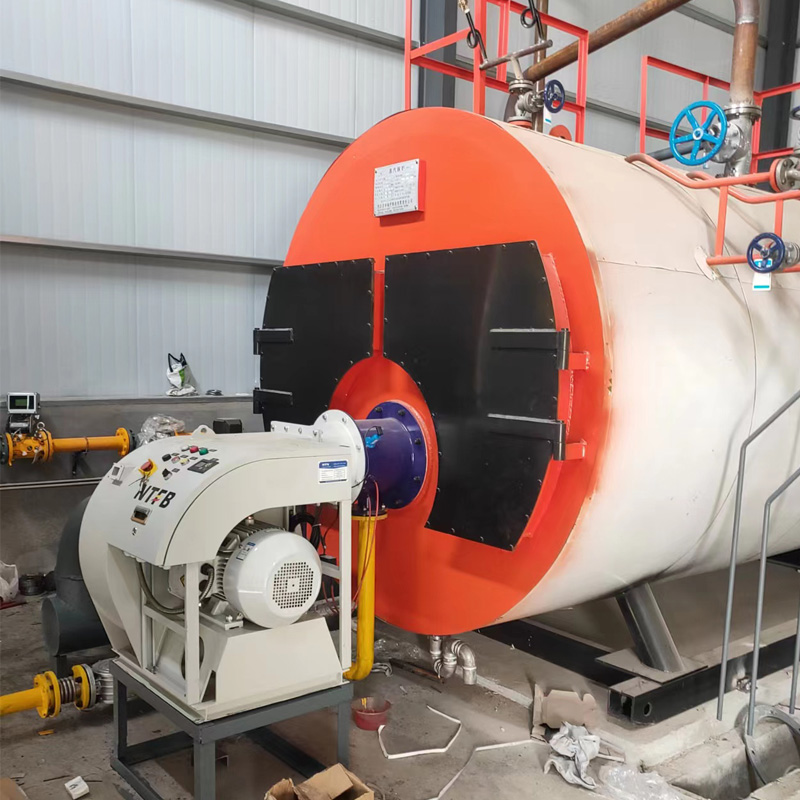
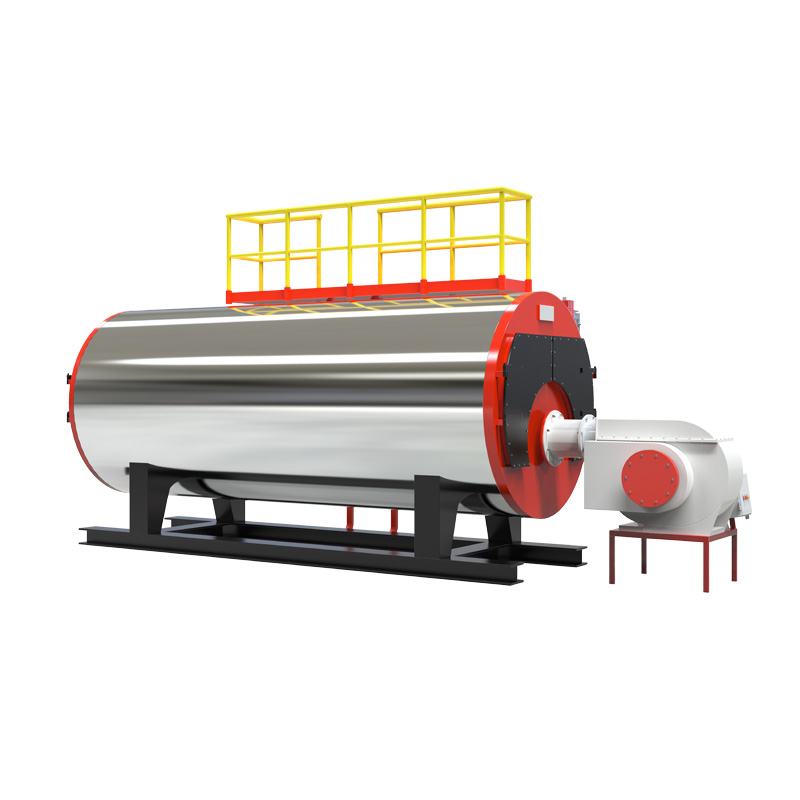
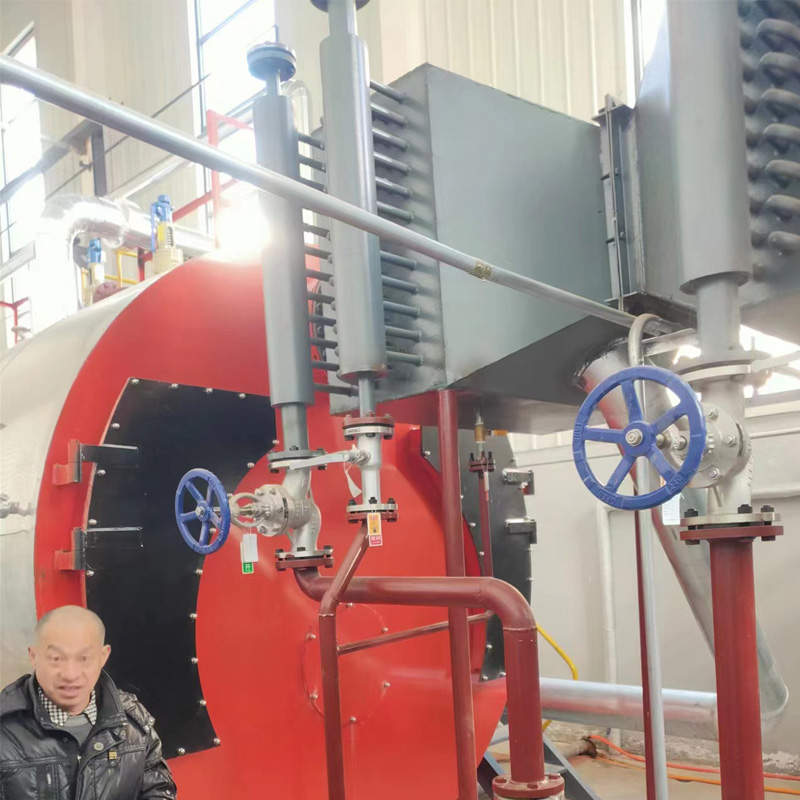
Industrial Oilfired Hot Water Boiler Factory Leading China Suppliers
Top China factory and suppliers of high-efficiency oil-fired hot water boilers. Rated thermal power 0.7-140 MW, working pressure 0.7-1.25MP, NOx emission ≤ 30mg. Compatible with diesel, heavy oil, and light oil for sustainable industrial heating.
SupplierHEBEI HONGZE BOILER MANUFACTURING CO., LTD.www.hzsteamboiler.com
Source categories
About this product
Product information from the supplier.
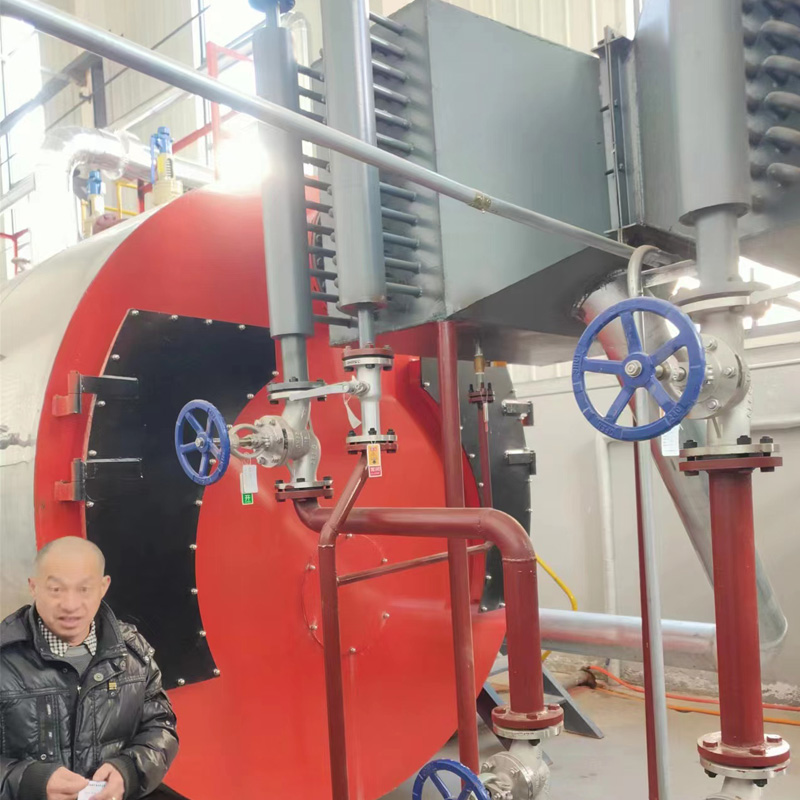
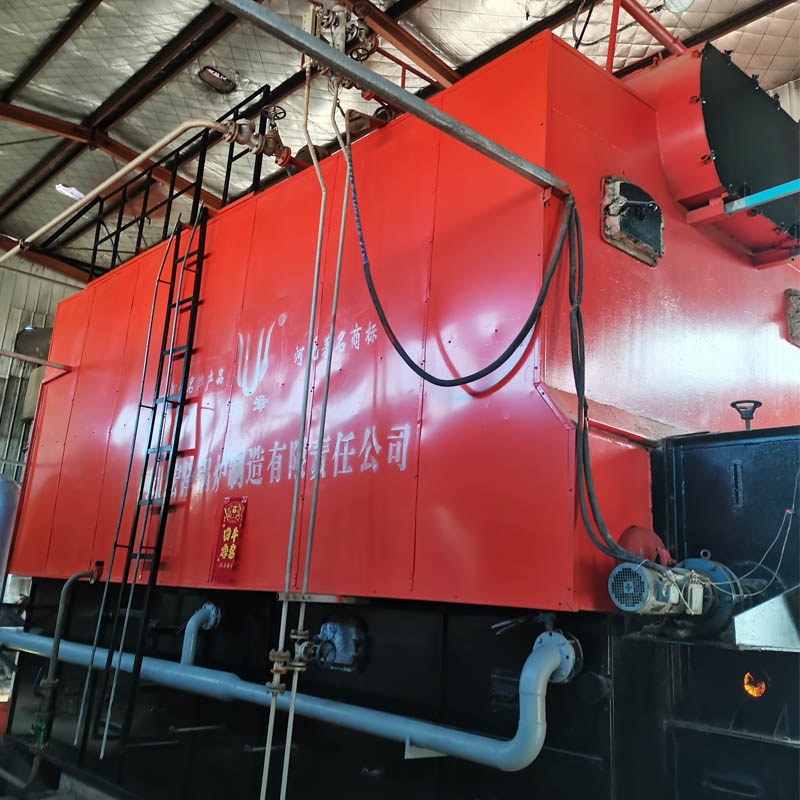
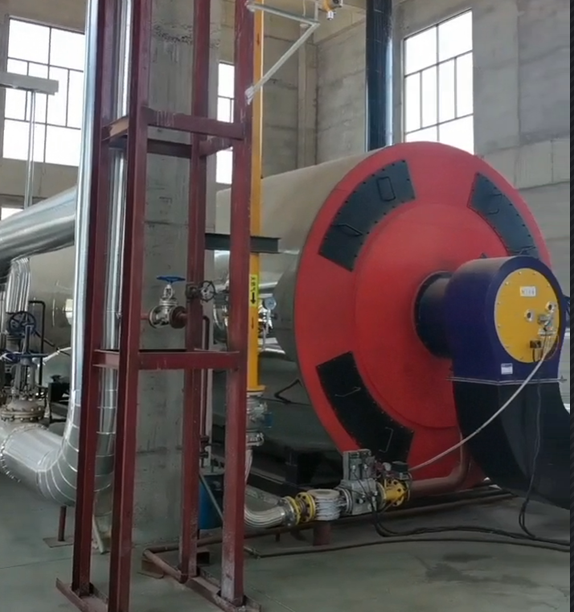
Our premium Oil-fired Hot Water Boilers are engineered for high-efficiency industrial heating, utilizing a sophisticated combustion process where oil is burned in the furnace to generate high-temperature flue gas. This thermal energy is continuously transferred to the circulating water within the pot, ensuring a steady and reliable supply of hot water for diverse industrial applications.
Designed with a focus on durability and thermal performance, these boilers integrate advanced furnace technology to optimize flue gas flow. This not only maximizes heat transfer efficiency but also significantly reduces internal wear and tear, providing a sustainable heating solution with a projected operational lifespan of up to 15 years.
Detailed Parameters
| Thermal Power Range | 0.7 MW - 46 MW | Working Pressure | 0.7 MPa - 1.25 MPa |
|---|---|---|---|
| Output Water Temp | 95℃ - 130℃ | Feeding Water Temp | 70℃ (Standard) |
| Max Thermal Efficiency | Up to 98.1% | Exhaust Gas Temp | 134℃ - 168.62℃ |
| Service Life | Up to 15 Years | Fuel Type | Industrial Oil |
| Quality Control | Double Inspection | Furnace Type | Advanced Efficiency Design |
Key Advantages
Strict Quality Control
Double inspection during raw material procurement and multi-layer production testing ensure the highest boiler quality.
15-Year Service Life
Robust engineering and high-grade materials ensure a long-term operational lifespan of up to 15 years.
High Thermal Efficiency
Achieving efficiency rates up to 98.1%, significantly reducing fuel consumption and operational costs.
Optimized Gas Flow
Advanced furnace design ensures reasonable flue gas velocity for maximum heat transfer and minimal wear.
Precision Engineering
Designed to maintain stable output temperatures ranging from 95℃ to 130℃ based on model specifications.
Source Traceability
Quality control starts from the source, ensuring every component meets rigorous industrial standards.
Product Gallery
Management Platforms
Quality Assurance
Full-cycle inspection from material sourcing to final factory testing.
Efficiency Monitoring
Precision control of flue gas flow to maximize thermal energy capture.
Maintenance Alerts
Systematic wear prevention to extend boiler life up to 15 years.
Thermal Control
Adaptive temperature management for output between 95℃ and 130℃.
Logistics Tracking
Secure packaging and professional transport for heavy industrial equipment.
Performance Audit
Regular efficiency benchmarks ensuring 90%+ thermal performance.
Investment Return Comparison
| Feature | Standard Boiler | Our Oil-fired Boiler |
|---|---|---|
| Thermal Efficiency | 80% - 85% | 93.8% - 98.1% |
| Operational Life | 5 - 8 Years | Up to 15 Years |
| Maintenance Cost | High (Frequent Wear) | Low (Optimized Flow) |
| Fuel Consumption | Standard | Reduced (High Efficiency) |
| Quality Check | Single Stage | Double Inspection |
Frequently Asked Questions
Q: What is the primary working principle of an oil-fired hot water boiler?
It works by burning oil in a furnace to create high-temperature flue gas. This heat is transferred to water circulating within the boiler, warming it up to the required temperature for industrial use.
Q: How do you ensure the quality of the boiler materials?
We implement a double-inspection system during raw material procurement and multi-stage quality checks throughout the production process, ending with rigorous factory testing.
Q: What is the expected service life of these boilers?
Thanks to advanced furnace designs that prevent flue gas wear and high-quality materials, our boilers are designed for a service life of up to 15 years.
Q: Can these boilers reach high thermal efficiency?
Yes, depending on the model, our boilers achieve thermal efficiency ratings from 93.8% up to 98.1%, ensuring minimal energy waste.
Q: What temperature ranges can the output water reach?
Depending on the selected model, the rated output water temperature ranges from 95℃ to 130℃ to suit various industrial heating requirements.
Q: How does the advanced furnace design benefit the user?
The optimized flue gas flow rate ensures maximum heat transfer efficiency while protecting the boiler's internal surfaces from excessive wear, reducing maintenance downtime.
Ready to Optimize Your Industrial Heating Efficiency?
Contact UsMore from this supplier
HEBEI HONGZE BOILER MANUFACTURING CO., LTD.