Image not available
Industrial manufacturing
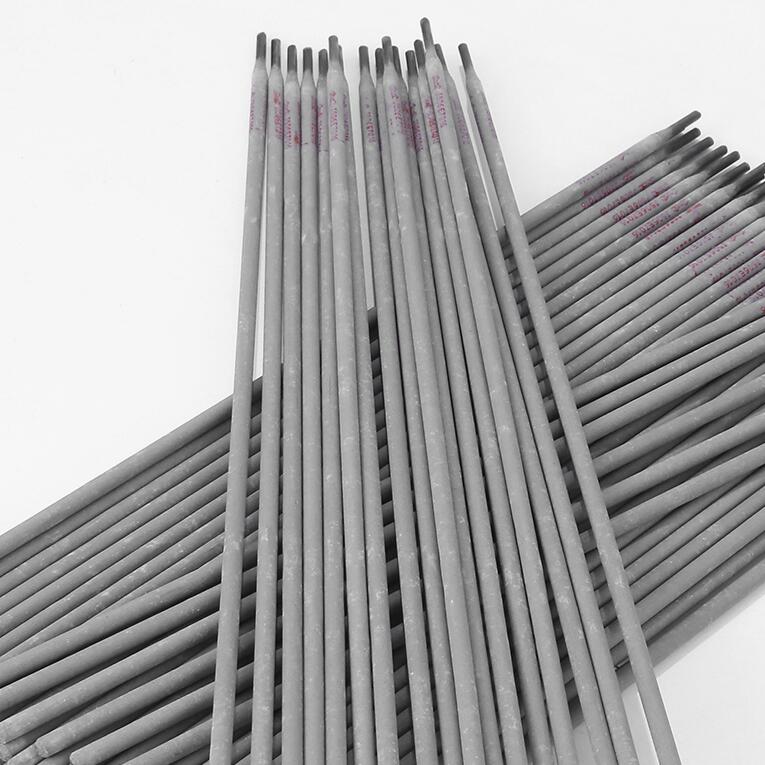
3.2mm 4mm 7018 welding rods electrodes
Iron powder type basic electrode GB/T 5117 E5018 AWS A5.1 E7018 ISO 2560-B-E4918 A
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
Iron powder type basic electrode
GB/T 5117 E5018
AWS A5.1 E7018
ISO 2560-B-E4918 A
AWS E7018 is basic coated iron powder low potassium hydrogen type electrode. Both AC and DC can be used and can be all-position welding. It can reach excellent welding performance, good arc stiffness,little spatter, easy slag removal and good weld appearance,high deposition efficiency.Weld metal has excellent plasticity and low temperature toughness
It can improve deposition efficiency because of the iron powder in the coating. Its arc is more stable with less spatter.It is easy to remove the residue. It can provide both beautiful welding line shape and good deposited metal mechanical performance.And the current can be AC or DC.It can be used for all position welding.
WELDING POSITIONS:
PA, PB, PC, PD, PE, PF.
X-ray flaw detection: Ⅰ level.
E7018 electrode is a carbon steel electrode with iron powder and low hydrogen potassium coating. Its arc stiffness is good, it is not easy to produce magnetic deflection blowing, the weld is fine and clean, with less spatter, easy to remove slag, and the weld has better low temperature. Toughness and crack resistance, dual-purpose DC, can be welded in all positions.
Any electrode marked with the end number of 5, 6 or 8 belongs to the low hydrogen type electrode. These electrodes are specially formulated to limit the amount of hydrogen in the final weld. Measures to reduce the hydrogen content should focus on cleaning weldments, joint design, and welding discontinuities. When welding with E7018 electrode, in order to prevent hydrogen from being deposited into the weld, the flux on the electrode should be kept dry. Once the package of welding rods is opened, the flux will begin to absorb moisture from the air. Exposure to air for about 4 hours, the performance of the flux coating will be impaired. If this happens, the electrode will no longer perform as it should, especially when welding high-strength and low-alloy steels. If you are using an electrode with the new H4R suffix, it will hold up well in air for 9h instead of 4h.
Since the E7018 welding rod is easy to absorb moisture, it is stored in a welding rod drying oven. The electrodes stored in the air can be re-baked at 350-400°C for 1h-2h. In order to restore the performance of its drug skin. Mild steel can be welded with unbaked E7018 electrodes, but the weld strength may not be high enough.
Need a quick quotation for E7018? Chat with us on WhatsApp or email info@steeltoolschina.com.
See the full E7018 low hydrogen electrodes range, or browse all welding electrodes.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.