Image not available
Industrial manufacturing
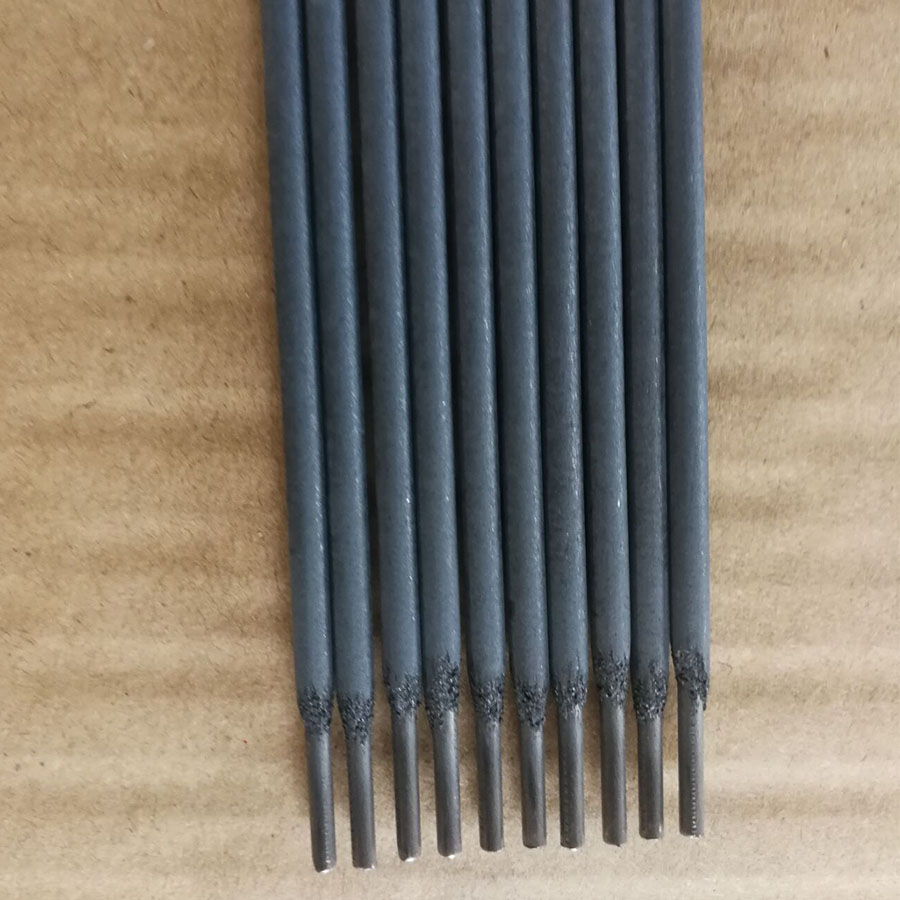
Cast Iron Welding Electrode Rod AWS ENiFe-CI
Z408 is the cast iron electrode with nickel iron alloy core and strong reduction of graphite coating . It can be used in AC and DC dual purpose, has stable arc,and is easy to operate. The electrode has the characteristics of high strength, good plasticity,
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
Cast Iron Welding Electrode Rod AWS ENiFe-CI.
Z408 is the cast iron electrode with nickel iron alloy core and strong reduction of graphite coating . It can be used in AC and DC dual purpose, has stable arc,and is easy to operate. The electrode has the characteristics of high strength, good plasticity, low linear expansion coefficient and so on. The crack resistance for grey cast iron is as much as that for Z308, while the crack resistance for nodular cast iron is more than Z308. For cast iron with higher phosphorus (0.2%P), it also has a good results and its tocutting performance is lower than Z308 andZ508 slightly. Z408 is used in the welding of gray iron and nodular cast iron for room
ATTENTION:
Before welding, the electrodes need to be baked for 1 hour with the temperature of 150±10℃ before using.
When welding ,it is appropriate to take narrow weld and each weld length should not exceed 50mm. Hammer the welding area lightly with a hammer immediately after welding in order to eliminate stress and prevent cracks.
Lower heat input is recommend.
Applicable process of cast iron welding rod
- Proper surface cleaning must be done before welding, and the welded joint should be obliquely cut into a U-shaped groove.
- Stop crack holes at both ends of the crack to prevent crack expansion during welding.
- When the angle of repair is not good, you can use WE100 welding rod to cold groove to form an effective U-shaped or V-shaped groove.
- Weld with as little current as possible, medium arc length, and slightly inclined to the welding direction.
- It is recommended to use short and thin welding beads and a narrow lateral swing welding torch to fill the weld joint before stopping arc welding. Usually no heat treatment is required and the parts are allowed to cool slowly.
Cast iron is an iron-carbon alloy with a carbon content greater than 2%. At present, more than 10 kinds of cast iron welding electrodes can be provided in China, which can be selected according to different cast iron materials, different cutting processing requirements and the importance of welding repair parts.
Cast iron is a material with poor weldability due to its high carbon content, uneven structure and low plasticity. Defects such as white spots, cracks, and pores are easy to occur during the welding process. Therefore, cast iron welding repairs require a high degree of welder technical proficiency. Cast iron welding repairs can be roughly divided into preheat welding and cold welding.
Need a quick quotation for Z408? Chat with us on WhatsApp or email info@steeltoolschina.com.
Compare our complete cast iron welding rods line, or view all welding electrodes.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.