Image not available
Industrial manufacturing
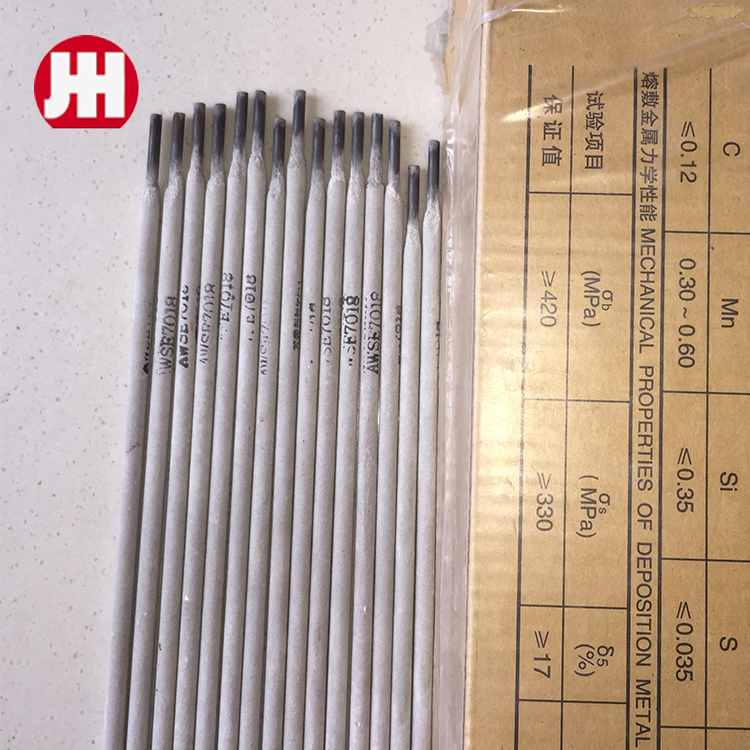
AWS E7018 Low Hydrogen Welding Rods China Factory Suppliers
High-strength AWS E7018 low hydrogen welding electrodes from a leading China factory. Our suppliers provide premium rods for mild and low alloy steel, ideal for bridges and construction.
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
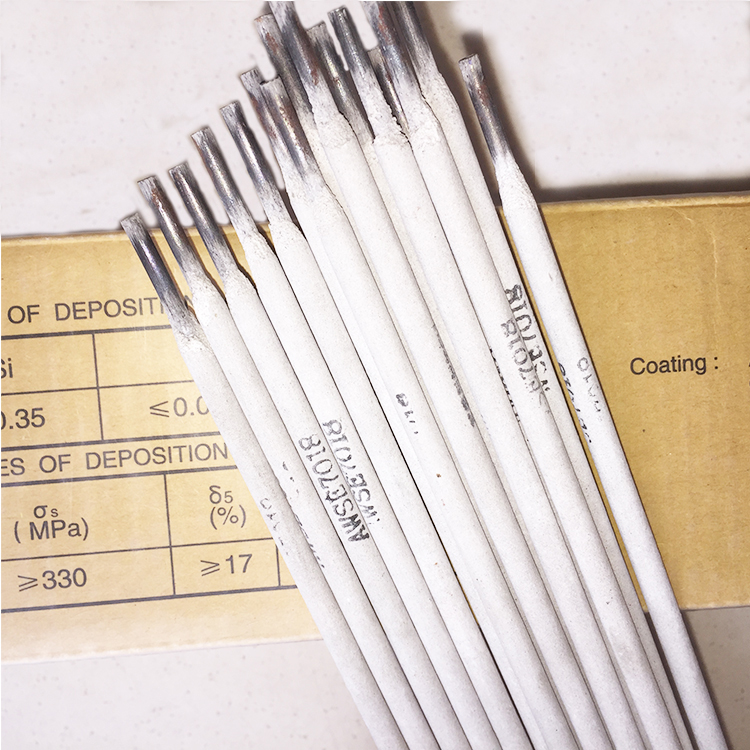
The AWS E7018 is a premium, multi-purpose low-hydrogen potassium electrode designed for high-strength applications in carbon and low-alloy steel welding. Engineered with an iron powder coating, this professional-grade welding rod optimizes deposition rates and minimizes the number of welding layers required, making it an industry standard for heavy-duty structural fabrication.
Ideally suited for critical infrastructure projects—including bridges, shipbuilding, pressure vessels, and mining equipment—the E7018 offers exceptional handling properties and stable arc performance. Whether utilized in construction or maintenance for machinery like bulldozers and agricultural equipment, it ensures high-integrity welds with superior mechanical properties and reduced risk of cracking.
Detailed Parameters
| AWS Classification | AWS A5.1: E7018 | Standard Compliance | GB/T 5117: E5018 / ASME SFA-5.1 |
|---|---|---|---|
| Coating Type | Low Hydrogen Potassium | Core Material | Carbon Steel with Iron Powder |
| Current Type | AC / DC Compatible | Welding Position | All-Position Welding |
| Baking Temp | 300°C (60 Minutes) | Storage Temp | 100°C - 150°C (Opened) |
| Application | Mild/Low Alloy Steel | Performance | High Strength & Low Spatter |
Key Advantages
Low Hydrogen Risk
Designed as a low-water hydrogen electrode to significantly reduce the risk of hydrogen-induced cracking in high-strength steel.
High Deposition Rate
The integrated iron powder in the coating increases welding efficiency and reduces the number of passes needed.
Excellent Formability
Delivers smooth bead appearance and excellent formability, ensuring professional aesthetic and structural finishes.
Stable Arc Performance
Features a stable tetrahedral arc opening with minimal spattering and high resistance to power supply fluctuations.
Versatile Application
Perfect for straight seams, transverse seams, corner seams, and specialized back welding requirements.
Operator Comfort
Low spatter and stable droplets provide higher safety and comfort for welders during long operational cycles.
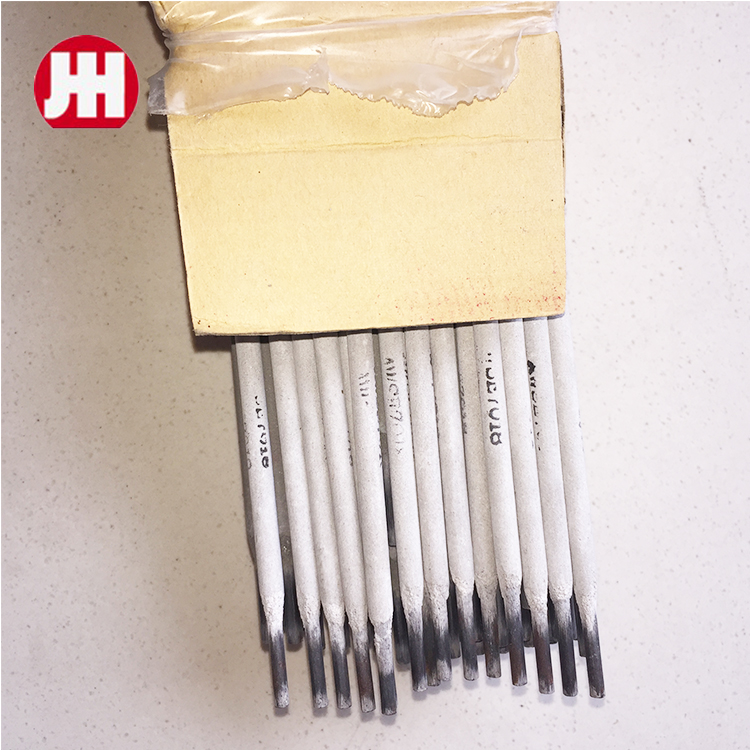
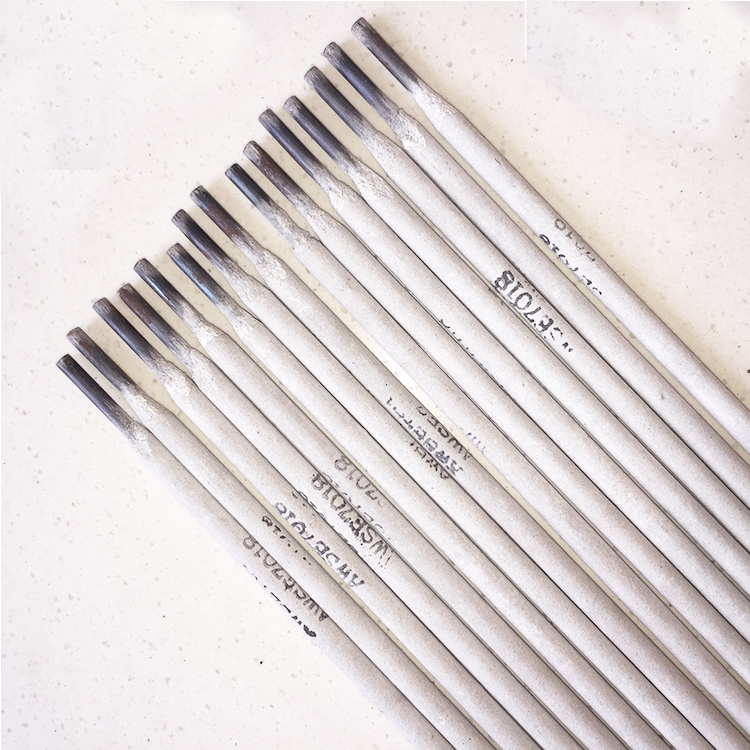
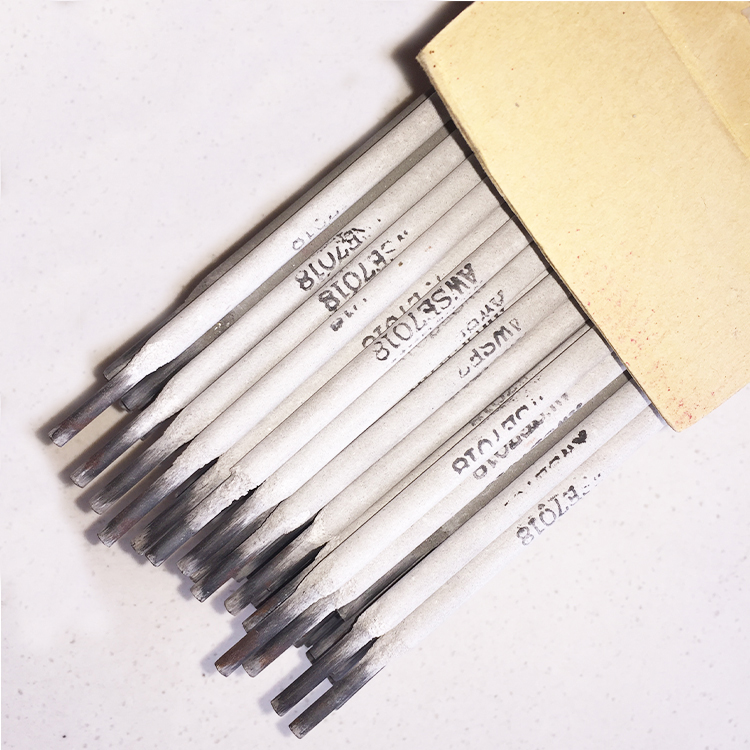
Product Gallery
Management Platforms
Surface Preparation
Ensure the base metal is free from water, dirt, and oil to prevent weld cracks and porosity.
Pre-use Baking
Bake electrodes at 300°C for 60 minutes to maintain low-hydrogen properties before welding.
Arc Length Control
Keep the arc length as short as possible to ensure stability and minimize spatter.
Weaving Technique
If swinging is required, ensure the range does not exceed 3 times the diameter of the electrode.
Storage Management
Opened rods should be stored in holding ovens at 100-150°C to prevent moisture absorption.
Arc Strike Method
Use the back-and-forward method during arc strike to prevent air holes or pit formation.
Investment Return Comparison
| Performance Metric | Standard Electrodes | AWS E7018 (Iron Powder) |
|---|---|---|
| Deposition Rate | Moderate | High (Iron Powder Enhanced) |
| Weld Strength | Standard | Extra High / Structural Grade |
| Spatter Level | Noticeable | Ultra-Low / Minimal |
| Labor Cost | Higher (More Layers) | Lower (Fewer Passes) |
| Crack Risk | Standard | Very Low (Low Hydrogen) |
Frequently Asked Questions
Q: Why is baking required for E7018 welding electrodes?
Baking removes moisture from the coating, ensuring the "low hydrogen" property. This is critical to prevent hydrogen-induced cracking in high-strength steel welds.
Q: What is the benefit of iron powder in the E7018 coating?
Iron powder increases the deposition rate, allowing the welder to fill joints faster and reduce the total number of welding layers required.
Q: Can E7018 be used for all-position welding?
Yes, the E7018 is designed for all-position welding, making it versatile for flat, horizontal, vertical, and overhead applications.
Q: Which materials are most suitable for E7018 electrodes?
It is primarily used for carbon steel and low alloy steel, such as 16Mn, and is ideal for heavy structural components like pressure vessels and bridges.
Q: What current can be used with the AWS E7018 rod?
The E7018 electrode is compatible with both AC (Alternating Current) and DC (Direct Current) welding machines.
Q: How should opened E7018 welding rods be stored?
Once the packaging is opened, electrodes should be stored in a drying oven at temperatures between 100°C and 150°C to prevent moisture re-absorption.
Ready to Upgrade Your Welding Quality?
Contact UsNeed a quick quotation for E7018? Chat with us on WhatsApp or email info@steeltoolschina.com.
Compare our complete E7018 low hydrogen electrodes line, or view all welding electrodes.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.