Image not available
Industrial manufacturing
AWS ENiCI Z308 Cast Iron Welding Rods China Factory Suppliers
High-quality AWS ENi-CI Z308 cast iron welding rods from a leading China factory. Featuring a pure nickel core for crack resistance and no preheating required. Trusted suppliers for industrial grade welding consumables.
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
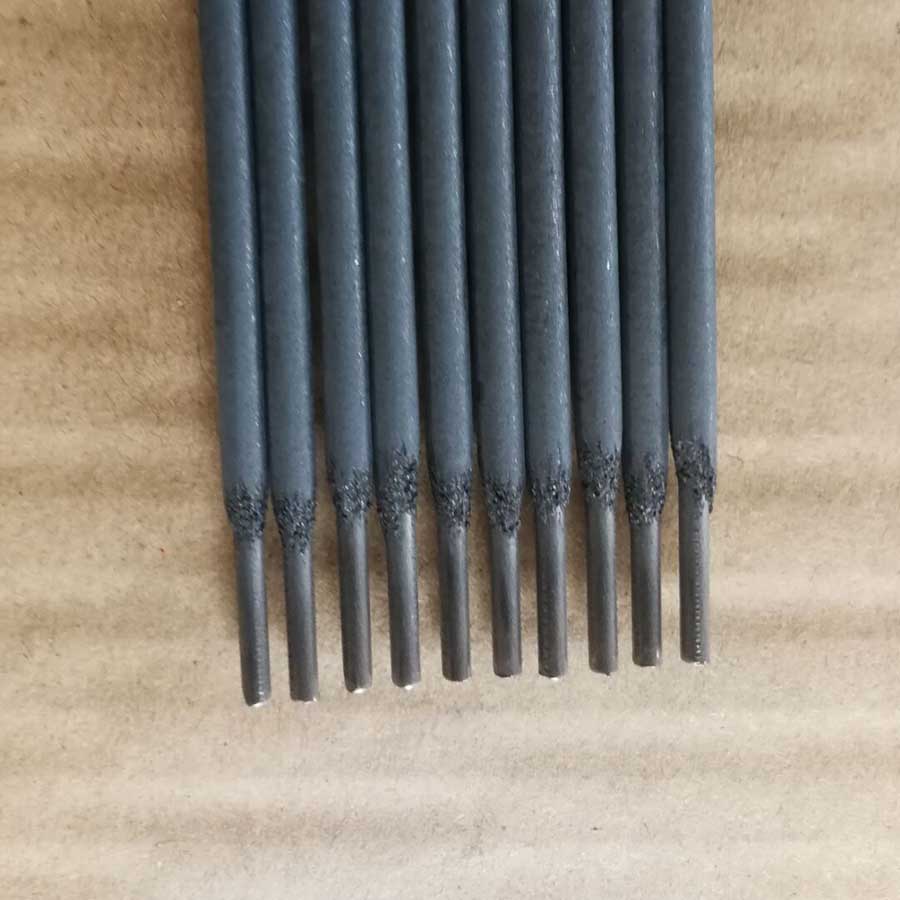
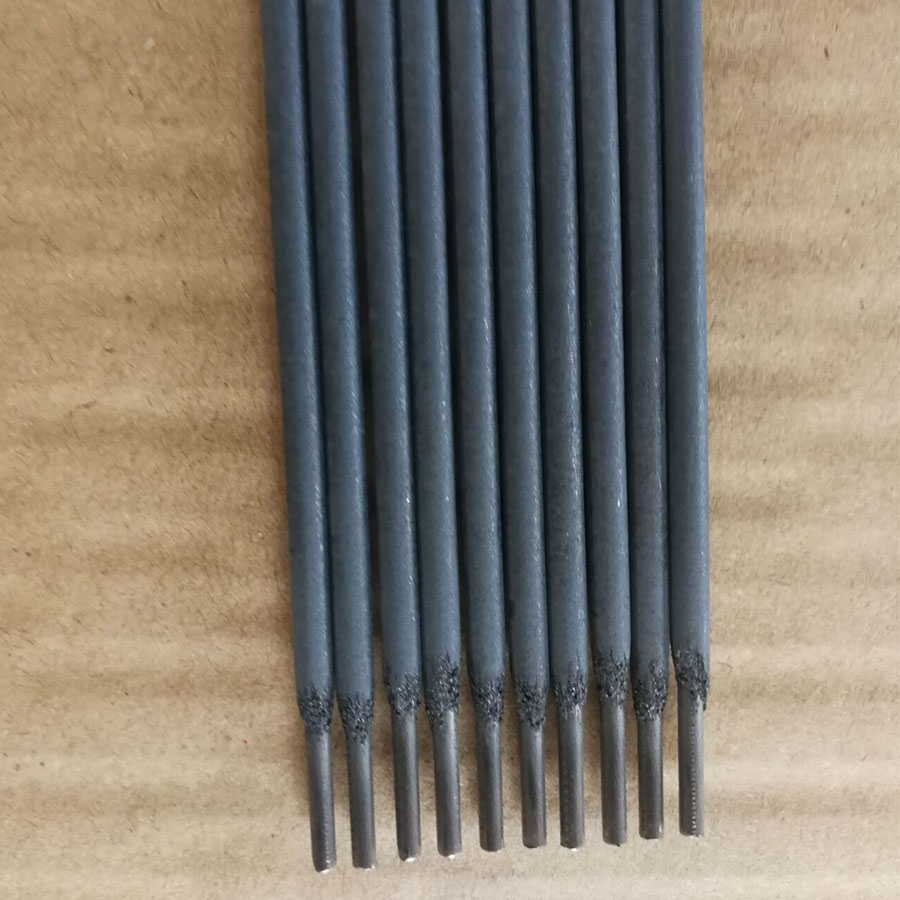
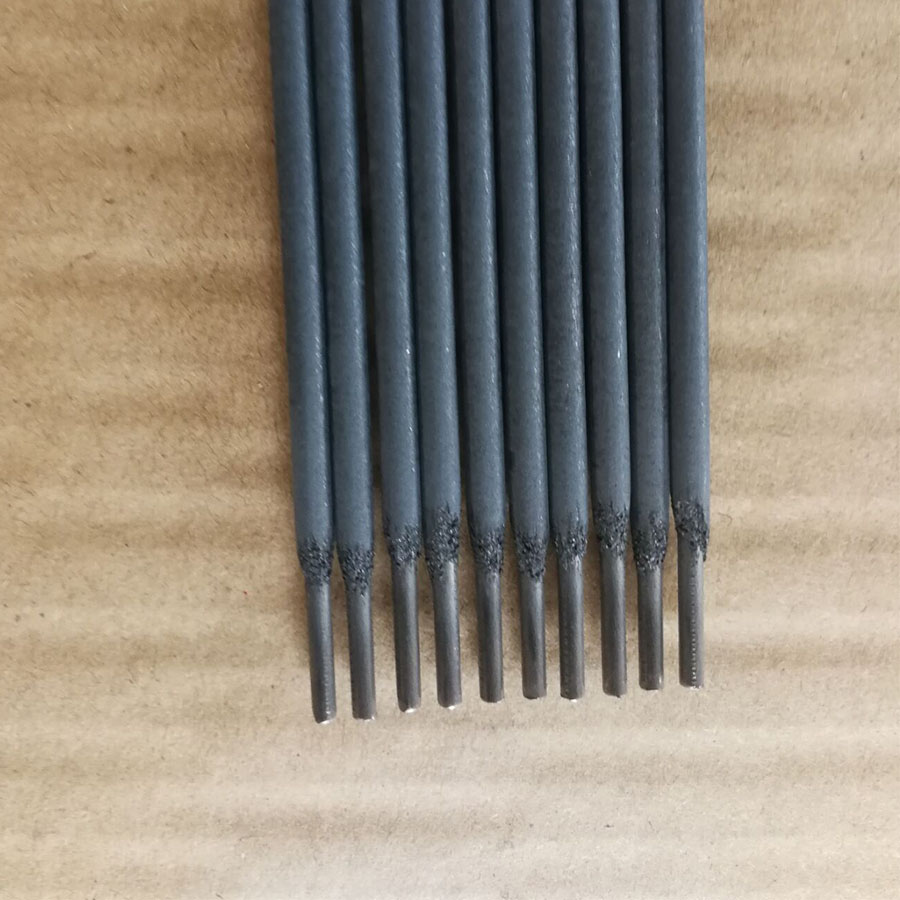
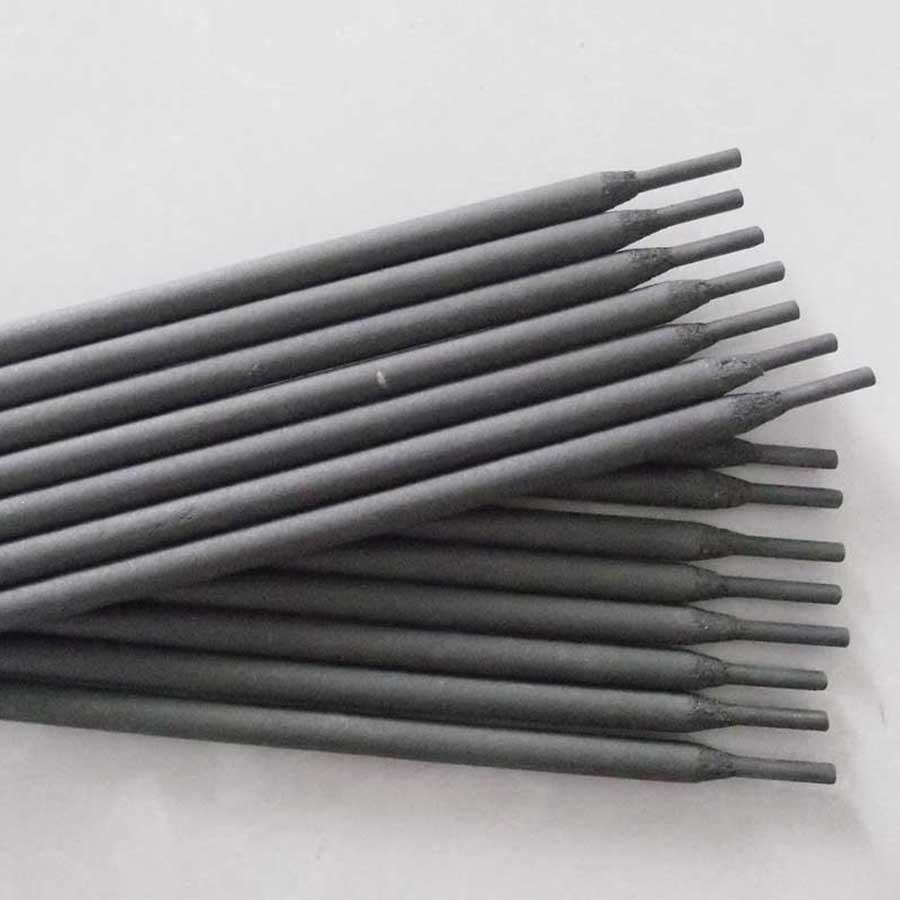
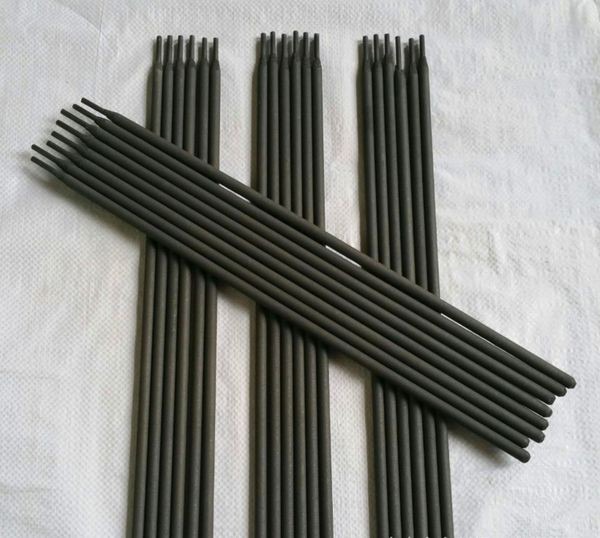
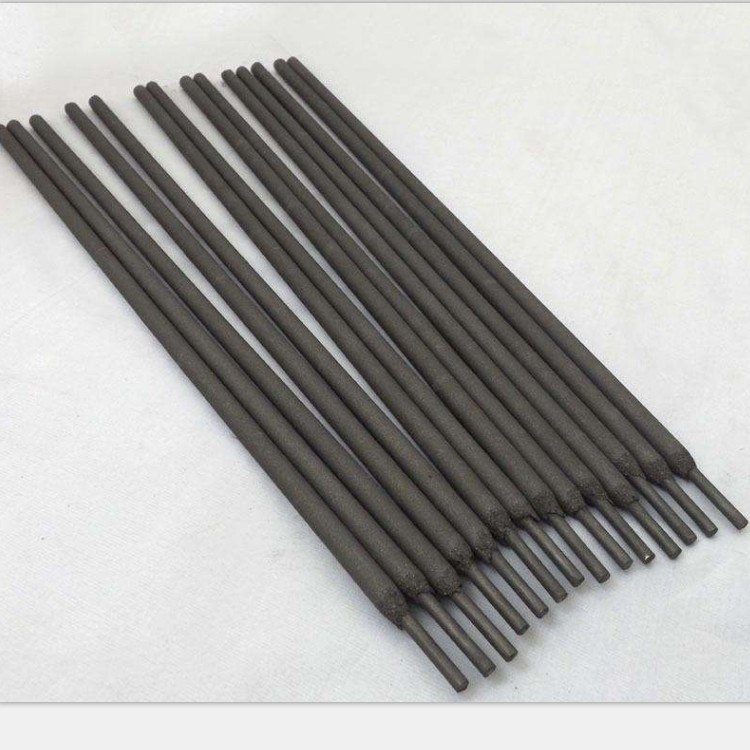
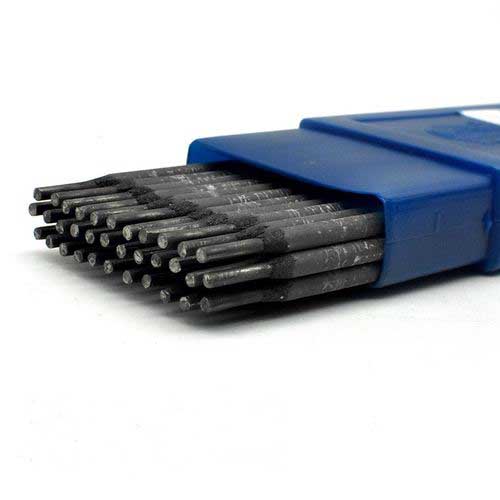
The AWS ENi-CI (Z308) Cast Iron Welding Rods are professional-grade welding consumables engineered for the precise repair and joining of cast iron components. Featuring a pure nickel core combined with a strong graphite-reducing coating, these electrodes ensure superior metallurgical compatibility, making them the ideal choice for industrial maintenance and precision tool manufacturing.
Designed for versatility and efficiency, the ENi-CI welding rods are compatible with both AC and DC power sources. Their advanced formulation eliminates the need for preheating the weldment, significantly reducing preparation time while providing exceptional resistance to cracking and excellent post-weld processability for machined parts.
Detailed Parameters
| AWS Classification | ENi-CI (Z308) | Core Material | Pure Nickel |
|---|---|---|---|
| Coating Type | Strong Graphite Reduction | Current Type | AC / DC Dual Purpose |
| Preheating | Not Required | Welding Positions | PA, PB |
| Baking Temperature | 150±10℃ | Baking Duration | 1 Hour |
| Flame Heating Temp | 700℃~850℃ | Max Heating Limit | 900℃ (Low Alloy Steel) |
Key Advantages
Crack Resistance
High-purity nickel core ensures exceptional resistance to brittle cracks during the cooling process.
Cold Welding Ready
Eliminates the need for weldment preheating, accelerating the overall repair workflow.
High Processability
Welded seams maintain excellent machining properties for precise finishing and fitting.
Dual Power Support
Fully compatible with both AC and DC welding machines for maximum site flexibility.
Impurity Control
Optimized for small current welding to reduce base metal penetration and white band width.
Stress Management
Easily eliminate welding stress through controlled hammering of the weld seam.
Product Gallery
Management Platforms
Quality Control
Rigorous raw material inspection ensuring pure nickel core consistency.
Thermal Management
Precision baking cycles at 150±10℃ to optimize electrode performance.
Stress Monitoring
Implementation of hammering techniques to avoid brittle weld cracks.
Deformation Control
Strict adherence to blue brittle temperature limits (300℃~500℃).
Annealing Protocol
Structured rectification before annealing to eliminate internal stress.
Heat Treatment
Calibrated flame straightening between 700℃ and 850℃.
Investment Return Comparison
| Performance Metric | Standard Rods | AWS ENi-CI (Z308) |
|---|---|---|
| Preheating Time | 2-4 Hours | 0 Hours (Immediate) |
| Crack Probability | Moderate to High | Very Low |
| Machinability | Difficult/Brittle | Excellent/Smooth |
| Operational Speed | Slow (Due to Heat) | Fast (Cold Welding) |
| Repair Success Rate | Standard | Superior Industrial Grade |
Frequently Asked Questions
Q: Do I need to preheat the cast iron before using AWS ENi-CI rods?
No, one of the primary advantages of the ENi-CI (Z308) electrode is that preheating the weldment is not necessary, allowing for efficient cold welding.
Q: How should the welding electrodes be prepared before use?
For optimal performance, electrodes should be baked for 1 hour at a temperature of 150±10℃ prior to application.
Q: What is the best way to prevent cracks in the weld seam?
You can eliminate welding stress and avoid cracks by carefully hammering the welding seam and utilizing small current welding to reduce impurity penetration.
Q: Which welding positions are supported by these rods?
The ENi-CI welding rods are designed for use in PA (flat) and PB (horizontal-vertical) welding positions.
Q: What temperature range should be used for flame straightening?
Flame straightening should typically be performed between 700℃ and 850℃ (fuchsia) and must not exceed 900℃ (bright red) for low alloy structural steel.
Q: Why is rapid cooling prohibited for hardenable welded parts?
Watering and rapid cooling are strictly prohibited because they can induce brittle cracks and adversely affect the mechanical properties of the steel.
Ready to Upgrade Your Welding Precision?
Contact UsNeed a quick quotation for Z308? Chat with us on WhatsApp or email info@steeltoolschina.com.
Browse the cast iron welding rods collection, or see every welding electrode we manufacture.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.