Image not available
Industrial manufacturing
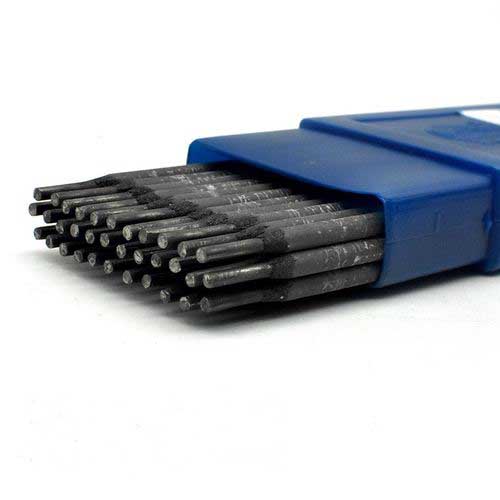
Z308 Pure Nickel Cast Iron Electrode AWS ENiCl China Suppliers Factory
Looking for reliable Z308 pure nickel cast iron electrodes? As leading China suppliers and factory, we provide AWS ENi-Cl rods for cold welding without preheating, featuring high crack resistance and AC/DC versatility.
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
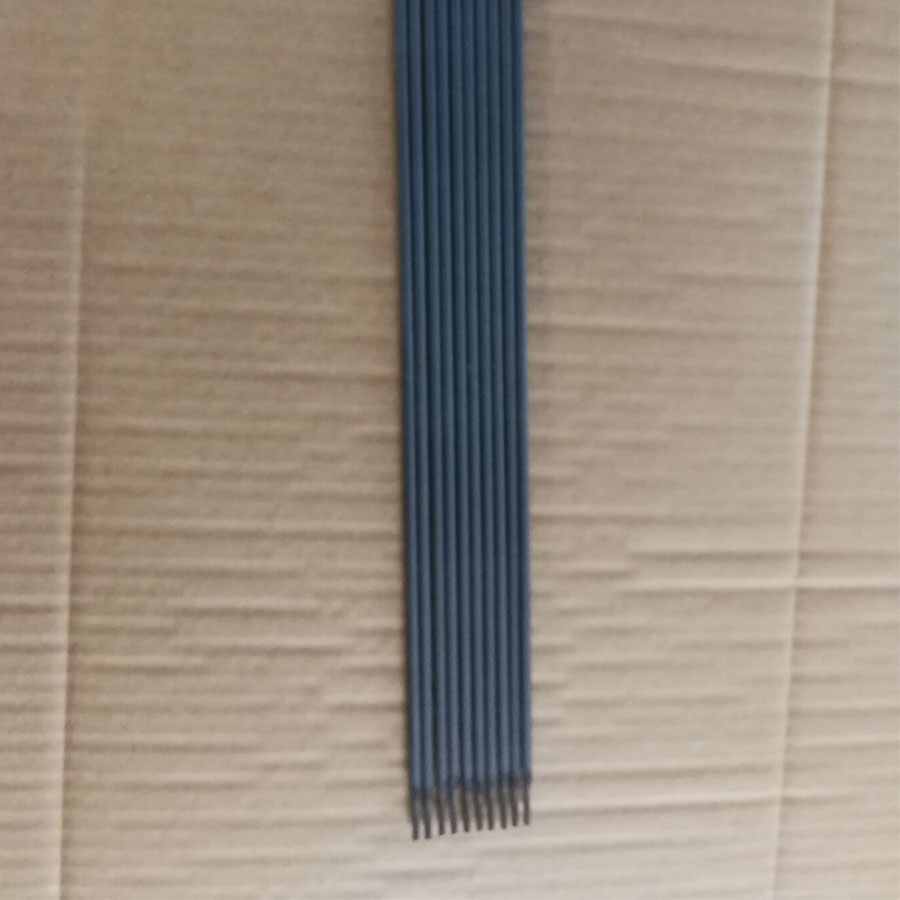
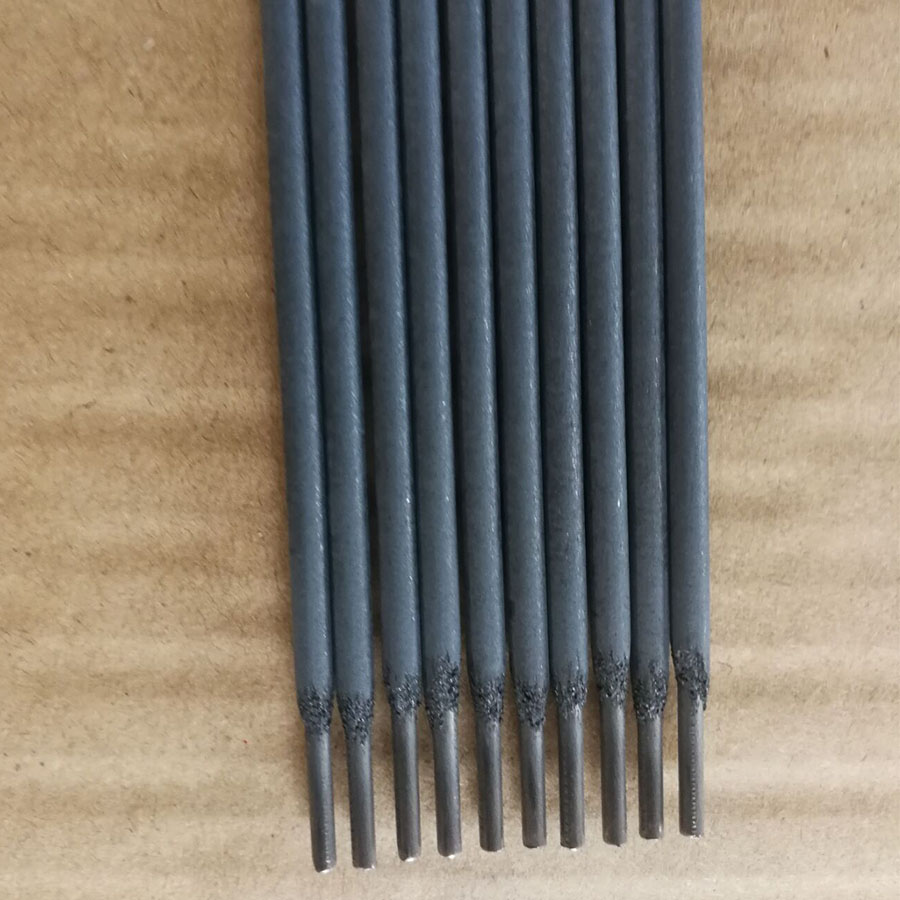
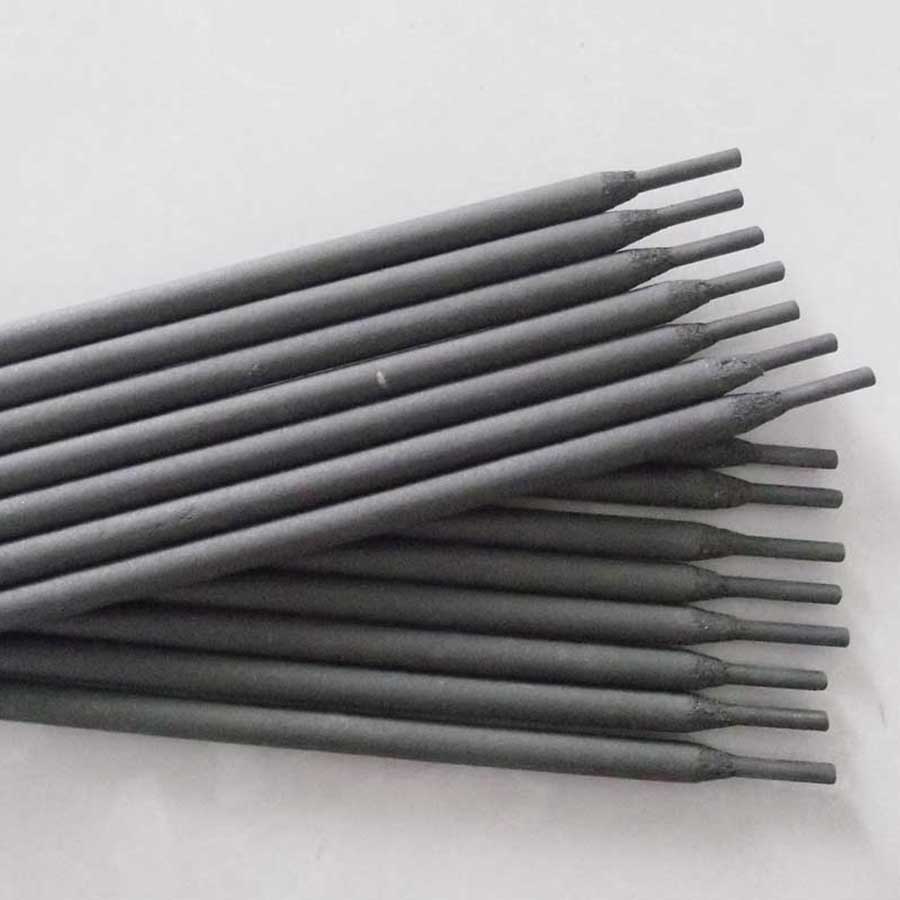
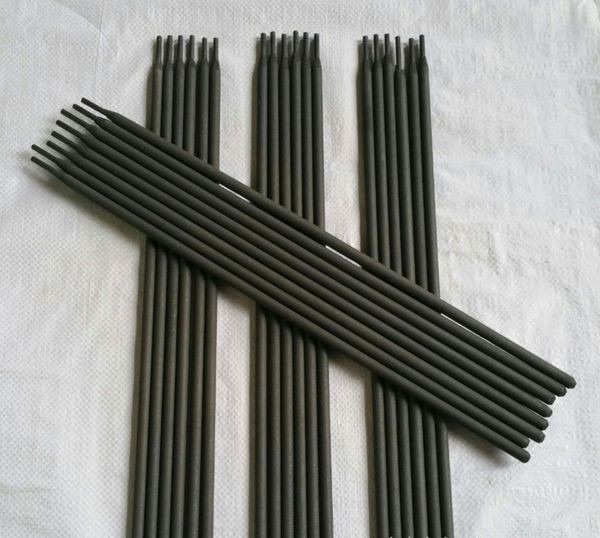
The Z308 Pure Nickel Cast Iron Electrode (AWS ENi-Cl) is a premium welding solution specifically engineered for the repair and maintenance of cast iron components. Featuring a pure nickel core and a strong graphite-type reduction coating, this electrode is designed for versatility, supporting both AC and DC currents to ensure seamless operation across various industrial environments.
Engineered for high-performance cold welding, the Z308 eliminates the need for preheating the weldment, significantly reducing preparation time. Its superior crack resistance and excellent post-weld processability make it the ideal choice for repairing engine shells, machine bases, and casting teeth where structural integrity and precision are paramount.
Detailed Parameters
| Product Model | Z308 / THZ308 | AWS Classification | ENi-Cl |
|---|---|---|---|
| Core Material | Pure Nickel | Coating Type | Strong reduction graphite type |
| Current Type | AC / DC Dual Purpose | Welding Position | PA, PB |
| Preheating Req. | Not Necessary | Baking Temp. | 150±10℃ (1 Hour) |
| Base Metal | Cast Iron (Fe-C Alloys) | Main Application | Cold Welding / Repair |
Key Advantages
High Crack Resistance
Specially formulated to prevent stress cracking in brittle cast iron base metals during the cooling process.
No Preheating Required
Saves significant time and energy by allowing direct cold welding without the need for heating the workpiece.
Excellent Machinability
The weld bead provides superior processability, allowing for easy grinding and machining after welding.
Dual Current Versatility
Fully compatible with both AC and DC welding machines, offering flexibility for all shop setups.
Low Impurity Penetration
Optimized for small current welding to minimize white band width and reduce base metal impurity penetration.
Broad Compatibility
Effective for various cast iron types, including engine covers, machine bases, and industrial gear housings.
Product Gallery
Management Platforms
Surface Preparation
Perform thorough cleaning and cut joints into U-shaped grooves to ensure maximum penetration.
Crack Prevention
Stop crack holes at both ends of the fracture to prevent further expansion during the welding process.
Thermal Control
Use small current welding and maintain short, thin beads to minimize heat input and stress.
Stress Relief
Hammer the weld seam immediately after welding to eliminate residual stress and avoid cracking.
Baking Protocol
Electrodes must be baked at 150±10℃ for 1 hour before use to ensure coating stability.
Cooling Process
Allow the finished parts to cool slowly at room temperature; typically, no post-heat treatment is required.
Investment Return Comparison
| Feature | Traditional Casting Repair | Z308 Pure Nickel Solution |
|---|---|---|
| Preheating Time | 3-8 Hours | Zero (Cold Welding) |
| Labor Cost | High (Complex heating) | Low (Direct Application) |
| Crack Risk | High (Thermal Shock) | Very Low (Pure Nickel) |
| Process Speed | Slow | Rapid / Efficient |
| Machinability | Difficult / Brittle | Excellent / Smooth |
Frequently Asked Questions
Q: Why is pure nickel recommended for cast iron welding?
Pure nickel is used because it remains ductile and does not form brittle carbides with the carbon in cast iron, which significantly reduces the risk of weld cracking.
Q: Is preheating absolutely unnecessary with Z308 electrodes?
Yes, Z308 is designed for cold welding. By using low current and short beads, you can avoid the costly and time-consuming preheating process.
Q: What is the purpose of hammering the weld seam?
Hammering helps to mechanically relieve the welding stress that builds up as the metal cools, preventing the formation of stress cracks in the cast iron.
Q: How should I prepare the joint before welding cast iron?
The surface must be thoroughly cleaned. The joint should be cut into a U-shaped groove, and stop-holes should be drilled at both ends of the crack to prevent extension.
Q: What current setting is best for Z308 electrodes?
It is recommended to use the smallest current possible. This reduces the width of the "white band" (brittle zone) and improves the overall ductility of the repair.
Q: Can Z308 be used on both AC and DC machines?
Yes, the Z308 electrode is dual-purpose, meaning it is fully compatible with both alternating current (AC) and direct current (DC) welding equipment.
Need Professional Cast Iron Welding Solutions?
Contact UsNeed a quick quotation for Z308? Chat with us on WhatsApp or email info@steeltoolschina.com.
Compare our complete cast iron welding rods line, or view all welding electrodes.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.