Image not available
Industrial manufacturing
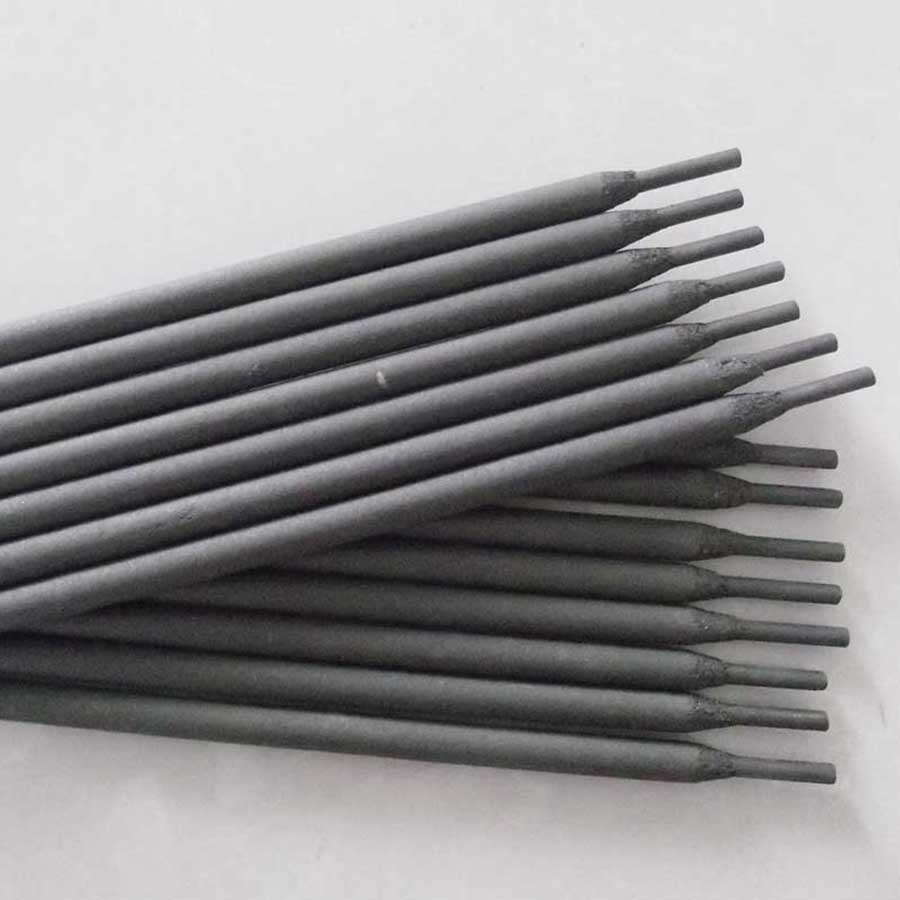
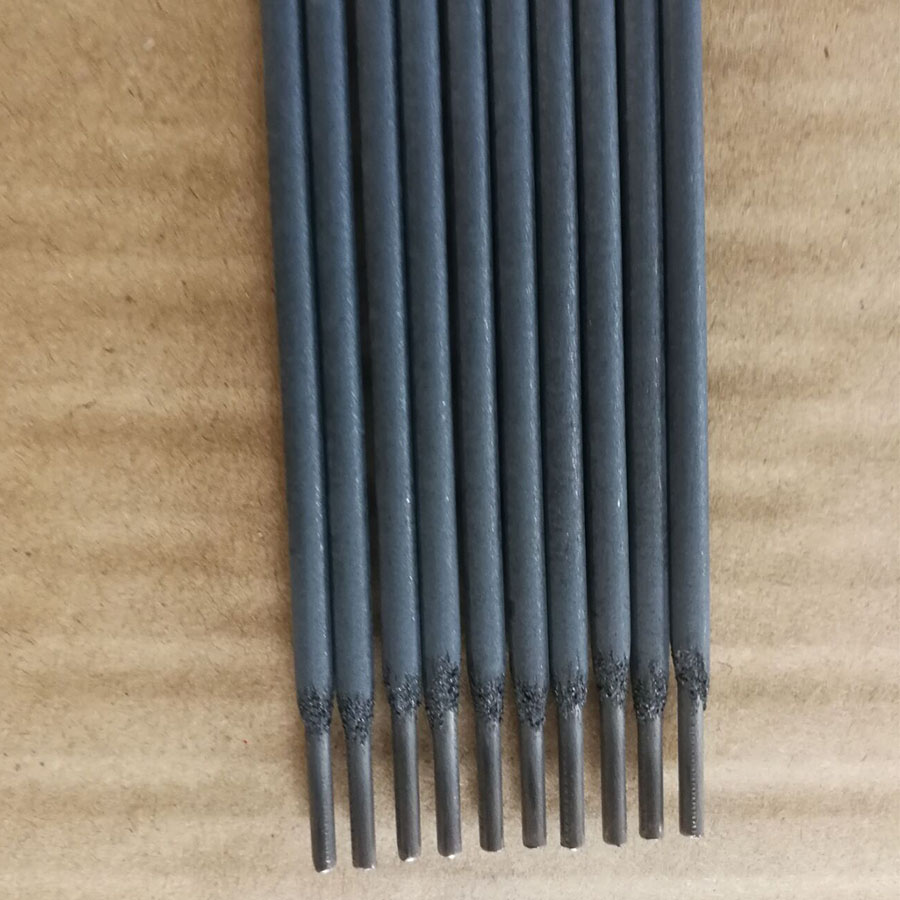
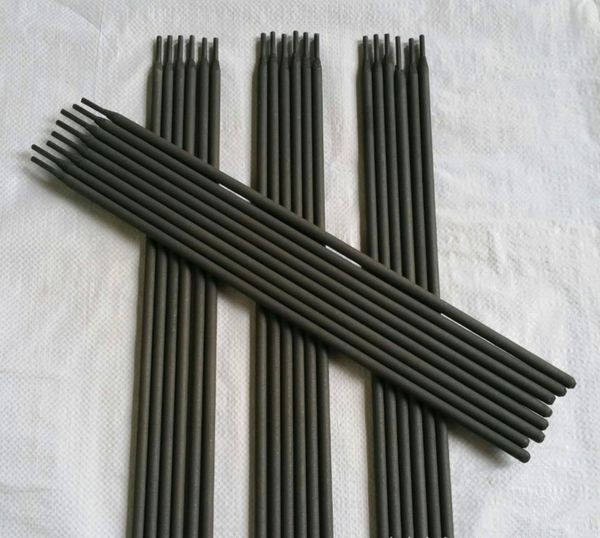
Z408 NickelIron Cast Iron Electrode AWS ENiFeCI China Factory Suppliers
Z408 is a premium cast iron electrode featuring a nickel iron alloy core and strong graphite reduction coating. Sourced from a leading China factory, our professional suppliers provide high-strength solutions for gray and nodular cast iron welding.
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
The Z408 Pure Nickel Cast Iron Electrode (AWS ENiFe-CI) is a high-performance welding solution engineered specifically for the challenging requirements of gray and nodular cast iron. Featuring a specialized nickel-iron alloy core and a potent graphite-reducing coating, the Z408 ensures a stable arc and exceptional operational ease, making it an industry standard for professional repair and fabrication.
Designed for versatility, this electrode is compatible with both AC and DC power sources. It is distinguished by its high strength, superior plasticity, and a low linear expansion coefficient, which significantly reduces the risk of thermal distortion. Whether dealing with standard cast iron or materials with higher phosphorus content (up to 0.2%P), the Z408 provides reliable crack resistance and structural integrity.
Detailed Parameters
| AWS Classification | ENiFe-CI | Product Model | Z408 |
|---|---|---|---|
| Core Material | Nickel-Iron Alloy | Coating Type | Strong Graphite Reduction |
| Current Type | AC / DC Dual Purpose | Applicable Materials | Gray & Nodular Cast Iron |
| Baking Temperature | 150±10℃ | Baking Duration | 1 Hour |
| Phosphorus Tolerance | Up to 0.2% P | Max Bead Length | 50mm per pass |
Key Advantages
Superior Crack Resistance
Offers exceptional crack resistance for nodular cast iron, exceeding the performance of Z308 electrodes.
Stable Arc Performance
Engineered for a smooth, stable arc that simplifies operation and reduces spatter during the welding process.
High Mechanical Strength
Combines high tensile strength with excellent plasticity to ensure durable, long-lasting weld joints.
Low Thermal Expansion
Low linear expansion coefficient minimizes internal stress and prevents post-weld deformation.
Versatile Compatibility
Highly effective for cast iron with higher phosphorus levels (0.2%P), providing consistent results.
Flexible Power Input
Fully compatible with both AC and DC welding machines for maximum workshop flexibility.
Product Gallery
Management Platforms
Surface Preparation
Thorough cleaning and U-shaped groove cutting are essential before welding begins.
Pre-Heating Protocol
Bake electrodes at 150±10℃ for 1 hour to ensure optimal performance and low hydrogen.
Stress Management
Lightly hammer the weld area immediately after welding to eliminate internal stress.
Heat Input Control
Maintain low heat input and use short, thin welding beads to prevent overheating.
Crack Prevention
Stop crack holes at both ends of the crack to prevent further expansion during the process.
Cooling Procedure
Generally no heat treatment is required; allow parts to cool slowly at room temperature.
Investment Return Comparison
| Performance Metric | Standard Electrodes | Z408 Nickel-Iron |
|---|---|---|
| Nodular Iron Resistance | Moderate | Excellent (High) |
| Phosphorus Tolerance | Low | High (up to 0.2%P) |
| Weld Plasticity | Standard | Superior |
| Arc Stability | Variable | Highly Stable |
| Risk of Cracking | Higher | Significantly Lower |
Frequently Asked Questions
Q: What is the primary use of Z408 welding electrodes?
Z408 electrodes are specifically designed for welding gray cast iron and nodular cast iron, providing high strength and excellent crack resistance.
Q: Why is baking necessary before using Z408 electrodes?
Baking at 150±10℃ for 1 hour removes moisture from the coating, ensuring a stable arc and preventing porosity in the weld.
Q: How do I prevent cracks when welding cast iron with Z408?
Use short beads (under 50mm), maintain low heat input, and lightly hammer the weld area immediately after finishing to relieve stress.
Q: Can Z408 be used on cast iron with high phosphorus content?
Yes, Z408 provides good results for cast iron containing up to 0.2% phosphorus, though cutting performance may be slightly lower than Z308.
Q: What is the recommended groove shape for Z408 welding?
It is recommended to obliquely cut the joint into a U-shaped groove for optimal penetration and strength.
Q: Is post-weld heat treatment required for Z408?
Usually, no post-weld heat treatment is required. The parts should simply be allowed to cool slowly at room temperature.
Looking for High-Quality Cast Iron Welding Solutions?
Contact UsNeed a quick quotation for Z408? Chat with us on WhatsApp or email info@steeltoolschina.com.
See the full cast iron welding rods range, or browse all welding electrodes.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.